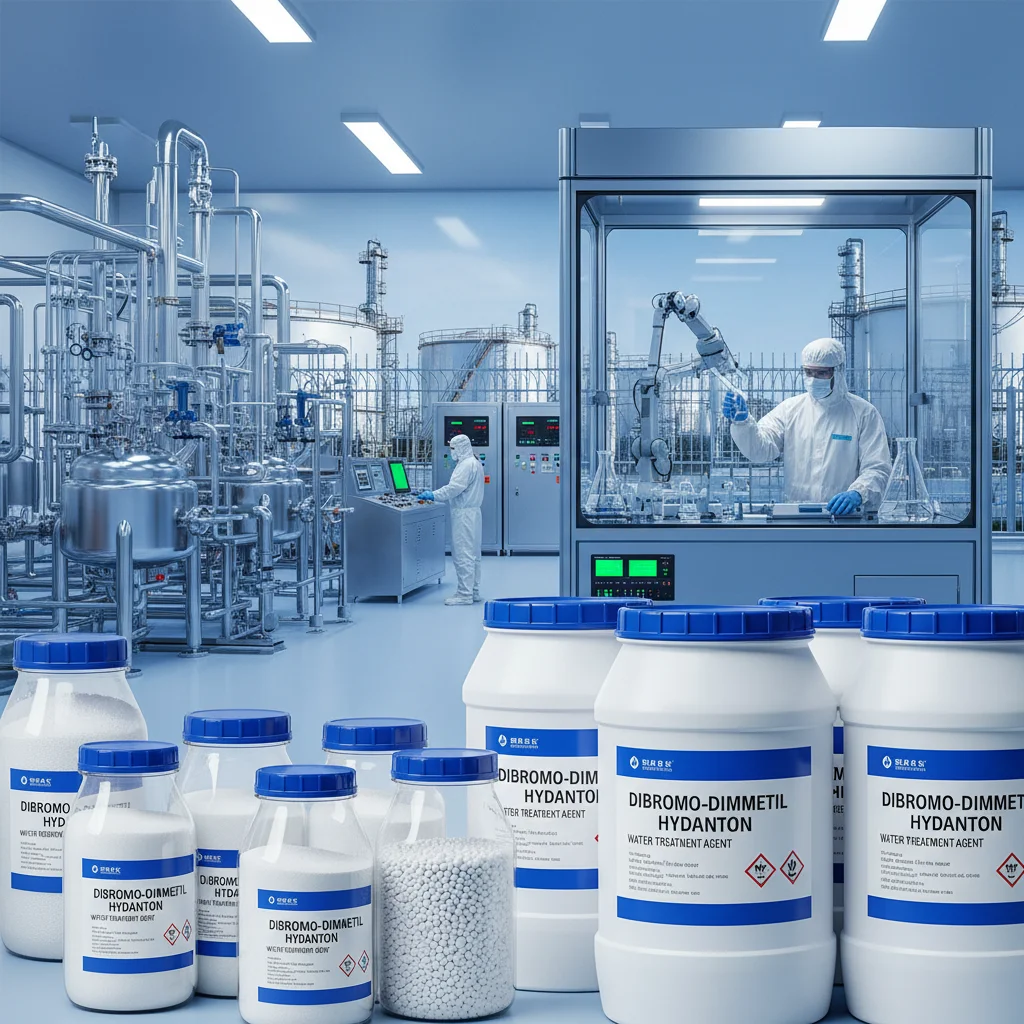
In the complex landscape of industrial microbiology, the demand for high-efficiency antimicrobial agents has led to the widespread adoption of specialized chemical solutions. The DBNPA product framework represents a critical shift toward precision water treatment, where the goal is to neutralize pathogens without compromising the structural integrity of the industrial system. By focusing on rapid action and controlled dissolution, these advanced chemicals ensure that cooling towers and process water remain free from hazardous biofilms.
Globally, the pharmaceutical and chemical manufacturing sectors face immense pressure to maintain sterile environments while adhering to strict environmental regulations. The implementation of a robust DBNPA product strategy allows facilities to reduce the risk of contamination, which otherwise leads to costly downtime and product degradation. With the rise of antibiotic-resistant bacteria in industrial water loops, the shift toward stabilized, high-purity chlorination agents has become a global industrial priority.
Understanding the technical nuances of these water treatment chemicals is essential for plant managers and engineers who seek to optimize heat exchange efficiency. By integrating a high-purity DBNPA product approach—specifically utilizing agents like Sodium Dichloroisocyanurate (SDIC) with 98%+ purity—industries can achieve a balance between potent disinfection and equipment longevity. This guide explores the technical specifications, applications, and future trends of these indispensable industrial chemicals.

Global Relevance of DBNPA product
The global industrial sector is currently grappling with the challenge of water scarcity and the increasing prevalence of waterborne biofilms. The DBNPA product landscape, particularly through agents like Sodium Dichloroisocyanurate (SDIC), provides a scalable solution to these problems. ISO standards for water quality highlight the need for stable chlorine release to prevent the proliferation of Legionella and other harmful microbes in large-scale industrial systems.
In the context of the pharmaceutical and fine chemical industries, the purity of water is non-negotiable. The adoption of high-purity chlorination chemicals ensures that process water does not introduce organic pollutants into the production line. By utilizing a stabilized DBNPA product approach, manufacturers can maintain a consistent pH range of 5.5–7.0, which is critical for preventing premature corrosion of stainless steel piping.
Defining the DBNPA product Standard
In simple terms, a DBNPA product standard in industrial water treatment refers to the use of highly efficient, fast-dissolving oxidizing agents designed to neutralize biological contaminants. Sodium Dichloroisocyanurate (SDIC) serves as a primary example, engineered specifically for rapid dissolution and a controlled release of active chlorine. This mechanism allows for the immediate eradication of pathogens while maintaining a residual disinfecting effect over time.
This approach connects directly to modern humanitarian and industrial needs by ensuring the safety of water used in manufacturing and wastewater pretreatment. When the active chlorine content is maintained at ≥60%, the chemical provides a powerful barrier against biofilm formation, which is the primary cause of heat exchange inefficiency in cooling towers. This technical precision transforms a simple chemical additive into a strategic asset for plant reliability.
Furthermore, the "standard" extends beyond the chemical formula to include the delivery method. Compatibility with automated dosing systems allows the DBNPA product logic to be applied with extreme precision, minimizing waste and reducing the environmental footprint of the treatment process. This systemic approach ensures that industrial facilities can meet rigorous safety benchmarks without sacrificing operational speed.
Core Components of DBNPA product Efficacy
The efficacy of a DBNPA product is primarily driven by its Purity and Composition. With a purity level of 98%+, the risk of introducing foreign minerals or impurities is virtually eliminated. This is crucial because impurities often lead to scaling in pipes, which can restrict flow and increase energy costs in large-scale water systems.
Another core factor is Stabilized Chlorine Release. Unlike conventional chlorine sources that may evaporate or degrade rapidly, the DBNPA product architecture ensures consistent performance even under fluctuating pH and temperature conditions. This stability is what allows industrial plants to maintain hygiene in extreme environments, such as high-temperature cooling loops.
Finally, Rapid Dissolution is the third pillar of efficiency. The ability of the chemical to dissolve quickly into the water stream ensures that there are no "dead zones" where bacteria can survive. This rapid action, combined with a moisture content of ≤3.0%, ensures that the product remains stable in storage but activates instantly upon application, providing a high return on investment for the operator.
Global Applications and Use Cases
The application of DBNPA product strategies is evident across diverse global industries. In cooling towers across North America and Europe, these chemicals are used to prevent microbial growth, ensuring that heat exchange efficiency is not compromised by organic sludge. By maintaining a sterile loop, plants can reduce their water consumption and energy overhead significantly.
In the pharmaceutical manufacturing hubs of Asia, particularly in the production of active pharmaceutical ingredients (APIs), process water treatment is critical. The DBNPA product method is employed to eliminate contaminants that could potentially compromise the chemical purity of the final drug product. This ensures that the manufacturing process adheres to global GMP (Good Manufacturing Practice) standards.
Efficiency Performance of DBNPA product Application Methods
Long-Term Value and Advantages
The long-term value of investing in a high-quality DBNPA product solution lies in the reduction of total operational expenditure (OPEX). By minimizing scaling and corrosion through precise pH control (5.5–7.0), the lifespan of expensive industrial equipment is extended. This reliability fosters trust in the facility's infrastructure and reduces the frequency of emergency repairs.
Beyond the financial gains, there is a significant sustainability angle. Using a stabilized chlorination agent reduces the volume of chemicals required to achieve the same disinfecting effect. This results in lower chemical runoff and a smaller environmental footprint. The safety and dignity of the workforce are also enhanced, as automated dosing of a stable DBNPA product reduces manual handling of hazardous materials.
Future Innovations in DBNPA product
The future of DBNPA product technology is moving toward "Smart Water Management." The integration of IoT sensors and AI-driven dosing algorithms will allow for real-time adjustments of chlorine levels based on the actual microbial load. This shift from scheduled dosing to demand-based dosing will maximize efficacy while minimizing chemical waste.
Furthermore, there is a growing trend toward "Green Chemistry" where the stability of these agents is enhanced through biodegradable carriers. Research is currently focusing on reducing the byproducts of chlorination further, ensuring that the water discharged from industrial sites is as benign as possible. These innovations align with global ESG (Environmental, Social, and Governance) goals.
Digital transformation is also impacting the supply chain. With the use of blockchain for traceability, users can now verify the purity levels (98%+) and origin of their DBNPA product shipments. This transparency is crucial for pharmaceutical companies that must provide a full audit trail for every chemical used in their production environment.
Overcoming Challenges in DBNPA product Deployment
One of the primary challenges in deploying a DBNPA product is the management of residual chlorine. If the levels are too high, they can cause corrosion; if too low, biofilms return. The solution lies in the implementation of automated ORP (Oxidation-Reduction Potential) controllers that maintain a precise equilibrium, ensuring that the active chlorine content remains effective but not destructive.
Storage and stability also present logistical hurdles. In humid climates, the moisture content must be kept below 3.0% to prevent clumping. The industry has solved this by adopting polyethylene-lined woven bags and fiber drums, which provide a superior moisture barrier. Proper storage protocols ensure that the chemical's potency is preserved from the factory to the dosing pump.
Lastly, regulatory compliance can be complex across different jurisdictions. Expert insights suggest that moving toward standardized documentation and third-party purity certifications can streamline the import/export process. By adhering to global standards, the deployment of a DBNPA product becomes a seamless part of the industrial operation.
Technical Comparison and Analysis of DBNPA product Specifications
| Parameter |
Industrial Standard |
Performance Impact |
Stability Score (1-10) |
| Active Chlorine |
≥60% |
Rapid pathogen neutralization |
9 |
| Product Purity |
98%+ |
Reduced scaling risk |
10 |
| Moisture Content |
≤3.0% |
Prevention of clumping |
8 |
| pH Range |
5.5–7.0 |
Corrosion prevention |
9 |
| Dissolution Rate |
Rapid |
Elimination of dead zones |
8 |
| Packaging |
PE-Lined Woven |
Long-term storage stability |
10 |
FAQS
The primary advantage is stability. Traditional chlorine can evaporate quickly or be affected by pH fluctuations. A DBNPA product strategy, using stabilized agents like SDIC, ensures a controlled release of active chlorine. This results in a more consistent disinfecting effect and reduces the frequency of chemical reapplications, making it more cost-effective and reliable for large industrial systems.
High purity means fewer inorganic impurities and minerals in the chemical. In industrial water systems, impurities often precipitate as scale on heat exchangers and pipes. By utilizing a DBNPA product with 98%+ purity, the risk of scaling is significantly reduced, which maintains optimal flow rates and prevents the premature degradation of metal surfaces.
Yes, it is specifically engineered for this purpose. Because of its rapid dissolution and predictable solubility, the DBNPA product logic fits perfectly into automated feeders. This allows plant managers to set precise concentrations, reducing the risk of human error and ensuring that the water remains within the ideal pH range of 5.5–7.0 at all times.
To maintain its active chlorine content and prevent clumping, the product should be stored in a cool, dry, and well-ventilated area. It is essential to keep the packaging—such as polyethylene-lined woven bags or fiber drums—sealed to ensure the moisture content remains below 3.0%. This preserves the chemical stability during long-term storage and transit.
Absolutely. In addition to cooling towers, the DBNPA product approach is highly effective for wastewater pretreatment. It helps in reducing hazardous organic byproducts and neutralizing pathogens before the water is discharged, ensuring that the facility meets environmental regulations and prevents the contamination of local water sources.
The ideal pH range for a 1% solution of these chemicals is typically between 5.5 and 7.0. Maintaining this range is critical because it optimizes the biocidal activity of the active chlorine while minimizing the corrosive effect on industrial piping. This balance is a key component of the DBNPA product efficiency model.
Conclusion
The implementation of a high-purity DBNPA product strategy, exemplified by the use of Sodium Dichloroisocyanurate (SDIC), provides an indispensable layer of protection for industrial water systems. By combining 98%+ purity, a stable active chlorine content of ≥60%, and a controlled pH range, industries can effectively eliminate biofilms and pathogens while extending the life of their critical infrastructure. This systemic approach not only ensures operational efficiency but also aligns with global standards of safety and environmental sustainability.
Looking forward, the integration of smart dosing and green chemistry will further refine the application of these chemicals, making industrial water treatment more precise and eco-friendly. For facilities seeking to optimize their water hygiene and reduce operational risks, transitioning to a stabilized, high-purity chemical regimen is the most viable path toward long-term reliability. To explore our full range of industrial water treatment solutions, visit our website: www.leache-chem.com.