

Email:
info@leachechem.com

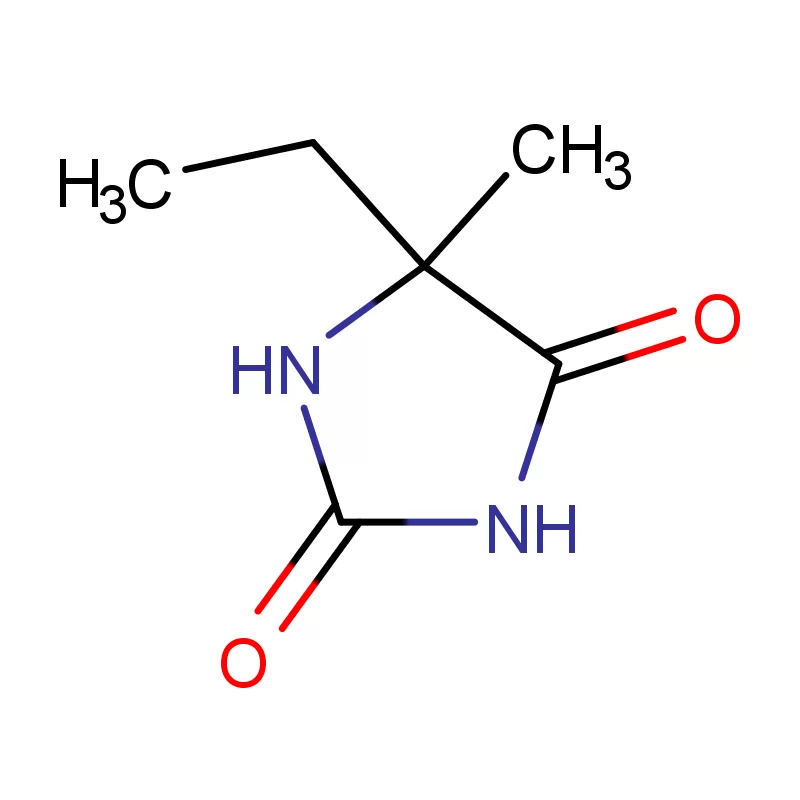
5-Ethyl-5-Methylhydantoin is a high-performance heterocyclic compound engineered specifically for the demanding requirements of the pharmaceutical and fine chemical industries. As a premium pharmaceutical intermediate, it serves as a critical building block in the synthesis of Active Pharmaceutical Ingredients (APIs), offering exceptional purity levels exceeding 99% to ensure maximum yield and stability in complex chemical reactions.
Beyond its primary use in API production, this versatile chemical demonstrates remarkable stability across various industrial processes. Its unique structural properties make it an indispensable component in the development of advanced antibiotics, anticonvulsants, and innovative agrochemical research, while also providing significant value in specialty polymer manufacturing and water treatment formulations.
| Chemical Purity | ≥99% | Physical Appearance | White crystalline powder |
|---|---|---|---|
| Moisture Content | ≤0.5% | Melting Point | 145–150°C |
| Product Category | Pharmaceutical Intermediates | Chemical Series | Hydantoin Series |
| Standard Packaging | 25 kg fiber drums | Liner Material | Double-layer polyethylene |
| Quality Standard | International Pharma Grade | Customization | 1 kg to 500 kg available |
With ≥99% purity, it minimizes impurities in synthesis, ensuring optimal performance in precision-driven API reactions.
Exhibits superior thermal and chemical stability, facilitating consistent results across diverse industrial processes.
Effective across pharmaceuticals, agrochemicals, water treatment, and advanced material science innovations.
Optimizes the bioavailability of compounds in agrochemical research for more efficient active ingredient delivery.
Every batch undergoes strict quality checks to ensure full compliance with international pharmaceutical standards.
Customizable packaging from 1 kg to 500 kg to meet specific storage and logistical requirements of global clients.
Precision monitoring for antibiotic and anticonvulsant production cycles.
Advanced chromatography platforms to guarantee ≥99% chemical purity.
Full documentation and tracking for every shipment to meet regulatory audits.
Strategic supply chain management for moisture-proof fiber drum shipping.
Real-time stock tracking for various packaging sizes from 1 kg to 500 kg.
Continuous alignment with global pharmaceutical intermediate standards.
| Performance Metric | Standard Grade | Premium Grade (Our Product) |
|---|---|---|
| Reaction Yield | Moderate | High Efficiency |
| Purification Cost | High (Extra Steps) | Low (Ready to Use) |
| Batch Consistency | Variable | Highly Consistent |
| Storage Stability | Standard | Enhanced (Moisture-Proof) |
| Regulatory Approval | Basic | International Compliance |
It is primarily used as a pharmaceutical intermediate for synthesizing Active Pharmaceutical Ingredients (APIs), particularly in the production of antibiotics and anticonvulsant medications.
A purity level of ≥99% ensures that side reactions are minimized, leading to higher yields and a cleaner final product, which is critical for meeting stringent pharmaceutical regulations.
Yes, it is also utilized in water treatment formulations, specialty polymer manufacturing, and agrochemical research to enhance the bioavailability of certain compounds.
Our standard packaging is 25 kg moisture-proof fiber drums with double-layer polyethylene liners, but we offer customized containers ranging from 1 kg up to 500 kg.
Every batch undergoes rigorous quality control checks, including purity analysis and moisture content testing, to ensure compliance with international pharmaceutical intermediate standards.
Absolutely. Its adaptability and stability make it an excellent choice for R&D in agrochemicals, particularly where enhancing the bioavailability of the active compound is required.