active pharmaceutical intermediates factory

Selecting a High-Performance active pharmaceutical intermediates factory

In today's volatile global supply chain, pharmaceutical procurement managers face a dual challenge: securing consistent material availability while adhering to increasingly stringent regulatory standards. The risk of batch variability or supply disruption can compromise entire production timelines. To mitigate these risks, partnering with an established active pharmaceutical intermediates factory that integrates history with modernization is essential.

Strategic Solution: Leache Chem Ltd addresses these precise industry pain points. Established in 1991, we have evolved from a traditional manufacturer into a world-class leader, becoming the first high-tech enterprise in China to realize the industrial production of 5,5-dimethylhydantoin and its derivatives.

Located in the Jingjin New Material Industrial Park, our facility operates not just as a production site, but as a strategic asset for our partners. By leveraging intelligent production workflows and automated packaging systems, we eliminate the common bottlenecks associated with manual handling. This commitment to modernization ensures that when you choose our facility, you are choosing a partner capable of supporting global demands across more than 50 countries with unwavering reliability.

Engineering Standards for our active pharmaceutical intermediates factory

Technical precision is the cornerstone of pharmaceutical safety. A superior active pharmaceutical intermediates factory must define its value through rigorous adherence to international standards and advanced engineering protocols. At Leache Chem, our operations are underpinned by a "Level A" R&D institution status within Hebei Province, ensuring that chemical synthesis meets the exact molar purity required for downstream applications.

We have engineered our facility to surpass baseline expectations, integrating digital storage solutions and standardized loading procedures to maintain chain-of-custody integrity. Below is a breakdown of how our technical infrastructure translates into tangible advantages for your supply chain.

Performance Metric Industry Significance Our Engineering Standard Advantage
Regulatory Compliance Market Access & Safety ISO9001, ISO14001, OHSAS18001, REACH, BSCI, NSF Certified Seamless entry into regulated markets (EU/USA) with zero compliance friction.
Production Consistency Batch-to-Batch Uniformity Intelligent Production & Automatic Packaging Elimination of human error, ensuring identical purity profiles across large volumes.
R&D Capability Innovation & Scaling Hebei Province Level 'A' R&D Institution Rapid prototyping of derivatives (e.g., Hydantoin series) for custom formulations.
Inventory Management Supply Chain Speed Digital Storage & Standardized Loading Real-time inventory visibility and faster logistical turnaround.

Maximizing ROI with an Advanced active pharmaceutical intermediates factory

Viewing your chemical supplier merely as a vendor limits your financial potential. A strategic alliance with a vertically integrated active pharmaceutical intermediates factory drives long-term Return on Investment (ROI) by reducing failure rates and streamlining procurement logistics. Leache Chem's independent brands—Bromiguard, Dr. Brom, and Leache—have sustained market presence for over 20 years, proving that quality consistency directly correlates with brand longevity and reduced total cost of ownership.

By consolidating production with a manufacturer that possesses deep capabilities in Hydantoin and Thiophene series products, partners reduce the administrative overhead of managing multiple vendors. Our intelligent manufacturing infrastructure lowers operational costs, savings which are passed on to our clients through competitive pricing without compromising the NSF-certified quality standards.

Related products

Reliable Dibromo 5 5 DimethylHydantoin exporter for Industry

Reliable Dibromo 5 5 DimethylHydantoin exporter for Industry

Selecting a reliable halogen-based biocide requires a deep understanding of the balance between oxidative power and material compatibility. In industrial water systems, the choice of a bromine-donor agent can dictate the long-term efficiency of cooling towers and the safety of pharmaceutical intermediate synthesis. The demand for stable, high-purity halogenated hydantoins has grown as operators seek alternatives to traditional liquid bleach or volatile chlorine gas. These organic solids provide a safer handling profile while maintaining the rigorous microbial control necessary for large-scale industrial operations. For procurement officers and plant engineers, identifying a qualified Dibromo 5 5 DimethylHydantoin exporter involves evaluating not just the chemical assay
High Purity Dibromo 5 5 DimethylHydantoin factory for API Synthesis

High Purity Dibromo 5 5 DimethylHydantoin factory for API Synthesis

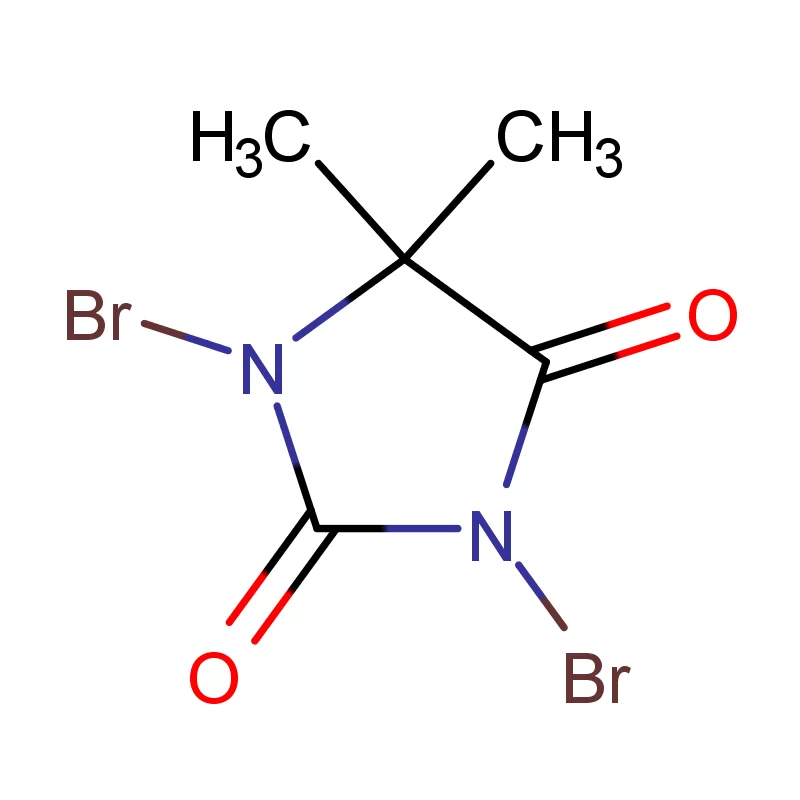
Selecting a reliable Dibromo 5 5 DimethylHydantoin factory is a critical decision for pharmaceutical and industrial water treatment enterprises that rely on precise halogenation. In the high-stakes environment of API synthesis and fine chemical manufacturing, the purity and stability of the bromine source can dictate the overall yield and the safety profile of the entire production batch. Dibromo 5,5-DimethylHydantoin DBDMH serves as a sophisticated brominating agent, offering a controlled release of active bromine compared to liquid bromine. This makes it indispensable for synthesizing sensitive intermediates where over-bromination or thermal instability could lead to costly process failures or safety risks.
Top Dibromo 5 5 DimethylHydantoin manufacturer for Water Treatment

Top Dibromo 5 5 DimethylHydantoin manufacturer for Water Treatment

The global demand for high-efficiency microbial control has led industries to seek a reliable Dibromo 5 5 DimethylHydantoin manufacturer capable of delivering consistent chemical purity. In the complex landscape of industrial water treatment, the ability to neutralize algae and bacteria while managing system corrosion is paramount for operational continuity. Understanding the role of advanced disinfectants is the first step toward optimizing large-scale aquatic systems. Modern industrial environments, from petrochemical plants to power generation facilities, face the constant threat of biofilm accumulation and scaling. A specialized Dibromo 5 5 DimethylHydantoin manufacturer provides the necessary chemical tools to maintain effluent quality and ensure compliance with strict environmental regulations.
Industrial Use of 5 5 DimethylHydantoin Sodium Salt product

Industrial Use of 5 5 DimethylHydantoin Sodium Salt product

The global industrial landscape is increasingly reliant on high-performance chemical stabilizers and oxidizing agents to maintain operational efficiency and system longevity. Among these, the 5 5 DimethylHydantoin Sodium Salt product serves as a critical component in the formulation of advanced water treatment chemicals, particularly those based on stabilized bromine. By providing a robust framework for active halogen delivery, it ensures that industrial systems remain free from biological contaminants and mineral deposits. In the context of modern pharmaceutical intermediates and fine chemicals, the demand for precision and stability is paramount.

If you are interested in our products, you can choose to leave your information here, and we will be in touch with you shortly.