Email:
info@leachechem.com

In the pharmaceutical and chemical synthesis sectors, the search for a reliable partner often hits a common roadblock: finding a balance between advanced innovation and supply chain consistency. Procurement managers and chemical engineers frequently struggle with suppliers who lack the regulatory certifications or the manufacturing scale to meet fluctuating global demands. Securing a dependable api intermediates supplier is not just about purchasing chemicals; it is about ensuring the integrity of your downstream products through a stable, compliant supply chain.
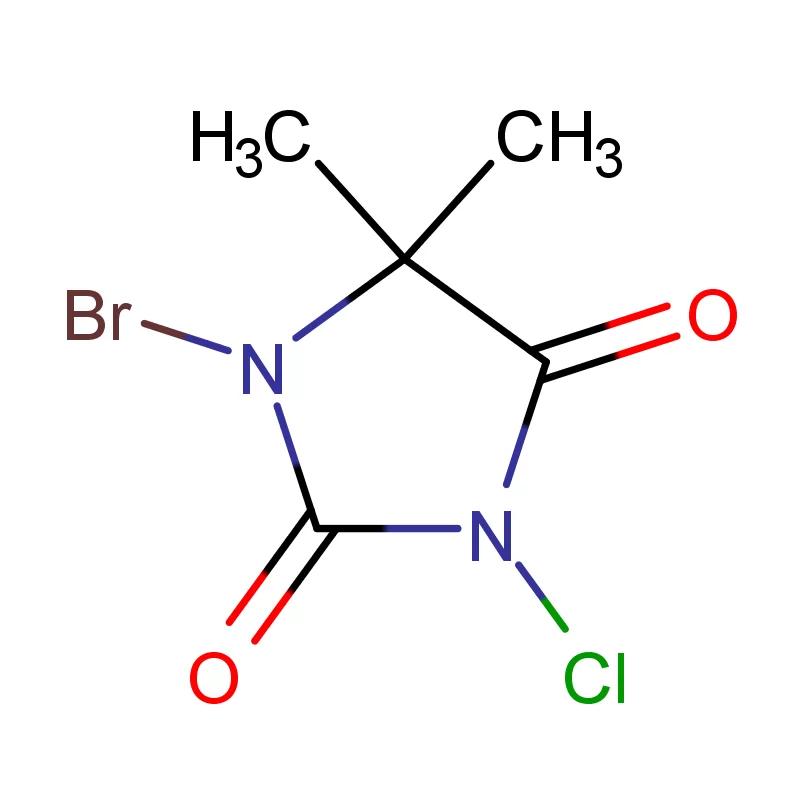
Since 1991, Leache Chem Ltd has addressed this industry-wide challenge by establishing itself as a world-class manufacturer. By evolving from a traditional factory to a high-tech enterprise, we have successfully bridged the gap between R&D and mass production. As the first enterprise in China to realize the industrial production of 5,5-dimethylhydantoin and its derivatives, we demonstrate the technical maturity required of a top-tier supplier. With a strategic presence in the Jingjin New Material Industrial Park and a robust global network serving over 50 countries, we offer the resilience and quality assurance that modern pharmaceutical supply chains demand.
Technical precision is the bedrock of pharmaceutical chemistry. When evaluating an api intermediates supplier, the focus must shift from simple capacity to process control, purity consistency, and environmental stewardship. At Leache Chem, we integrate intelligent production systems with rigorous quality frameworks to meet the exacting standards of the global market.
Our facility employs automatic packaging and digital storage solutions to minimize human error and contamination risks. Backed by our status as a Hebei Province Level 'A' R&D Institution, we maintain strict control over critical intermediates like hydantoin and thiophene series products. The table below outlines how our engineering standards translate into tangible advantages for our partners.
| Performance Metric | Industry Significance | Our Engineering Standard | Client Advantage |
|---|---|---|---|
| Regulatory Compliance | Ensures market access and safety. | ISO9001, NSF, & REACH Certified | Full traceability and seamless entry into regulated markets (US/EU). |
| Production Consistency | Reduces batch-to-batch variation. | Intelligent Production & Digital Storage | Uniform product quality reducing the need for reprocessing. |
| Environmental Responsibility | Critical for sustainable supply chains. | ISO14001 & OHSAS18001 | Mitigates supply disruption risks due to environmental audits. |
| R&D Capability | Adaptability to new formulations. | Level 'A' R&D Institution | Rapid scaling of niche derivatives like 5,5-dimethylhydantoin. |
Beyond the immediate cost per kilogram, the true value of an api intermediates supplier lies in risk mitigation and brand longevity. Partnering with a manufacturer that possesses over two decades of market presence—exemplified by our enduring brands 'Bromiguard', 'Dr. Brom', and 'Leache'—translates into a direct competitive advantage. Stability in the supply of precursors like hydantoin prevents costly production halts and reformulation delays.
By leveraging our win-win cooperation model and standardized loading protocols, our clients experience reduced lead times and lower logistical overheads. This efficiency allows pharmaceutical manufacturers to allocate resources toward drug development rather than supply chain firefighting. The chart below illustrates the comparative efficiency gains realized when utilizing our intelligent production ecosystem versus traditional manual processing.
Related products
Top Selling Products