Email:
info@leachechem.com

Sourcing reliable sanitation and cleaning products requires more than just finding a supplier; it demands a partner who understands the intricate balance between chemical efficacy and consumer safety. For procurement managers and distributors facing the challenge of inconsistent product quality or supply chain disruptions, identifying a manufacturing base with deep-rooted expertise is paramount. Leache Chem Ltd emerges as the definitive solution to these challenges, leveraging over three decades of industry leadership to provide stability and innovation.
Since 1991, we have established ourselves as a world-class leader in the manufacturing of hydantoin and its derivatives, the core active ingredients essential for high-performance cleaning tablets. As the owner of the independent brand 'Bromiguard', our facility is not merely a production line but the origin point of quality. By integrating intelligent production systems with international authoritative certifications such as ISO9001, ISO14001, and NSF, we ensure that every batch meets rigorous global safety standards. Our capacity to serve clients across more than 50 countries demonstrates our ability to handle complex, large-scale demands while maintaining the personal touch of a dedicated manufacturing partner.
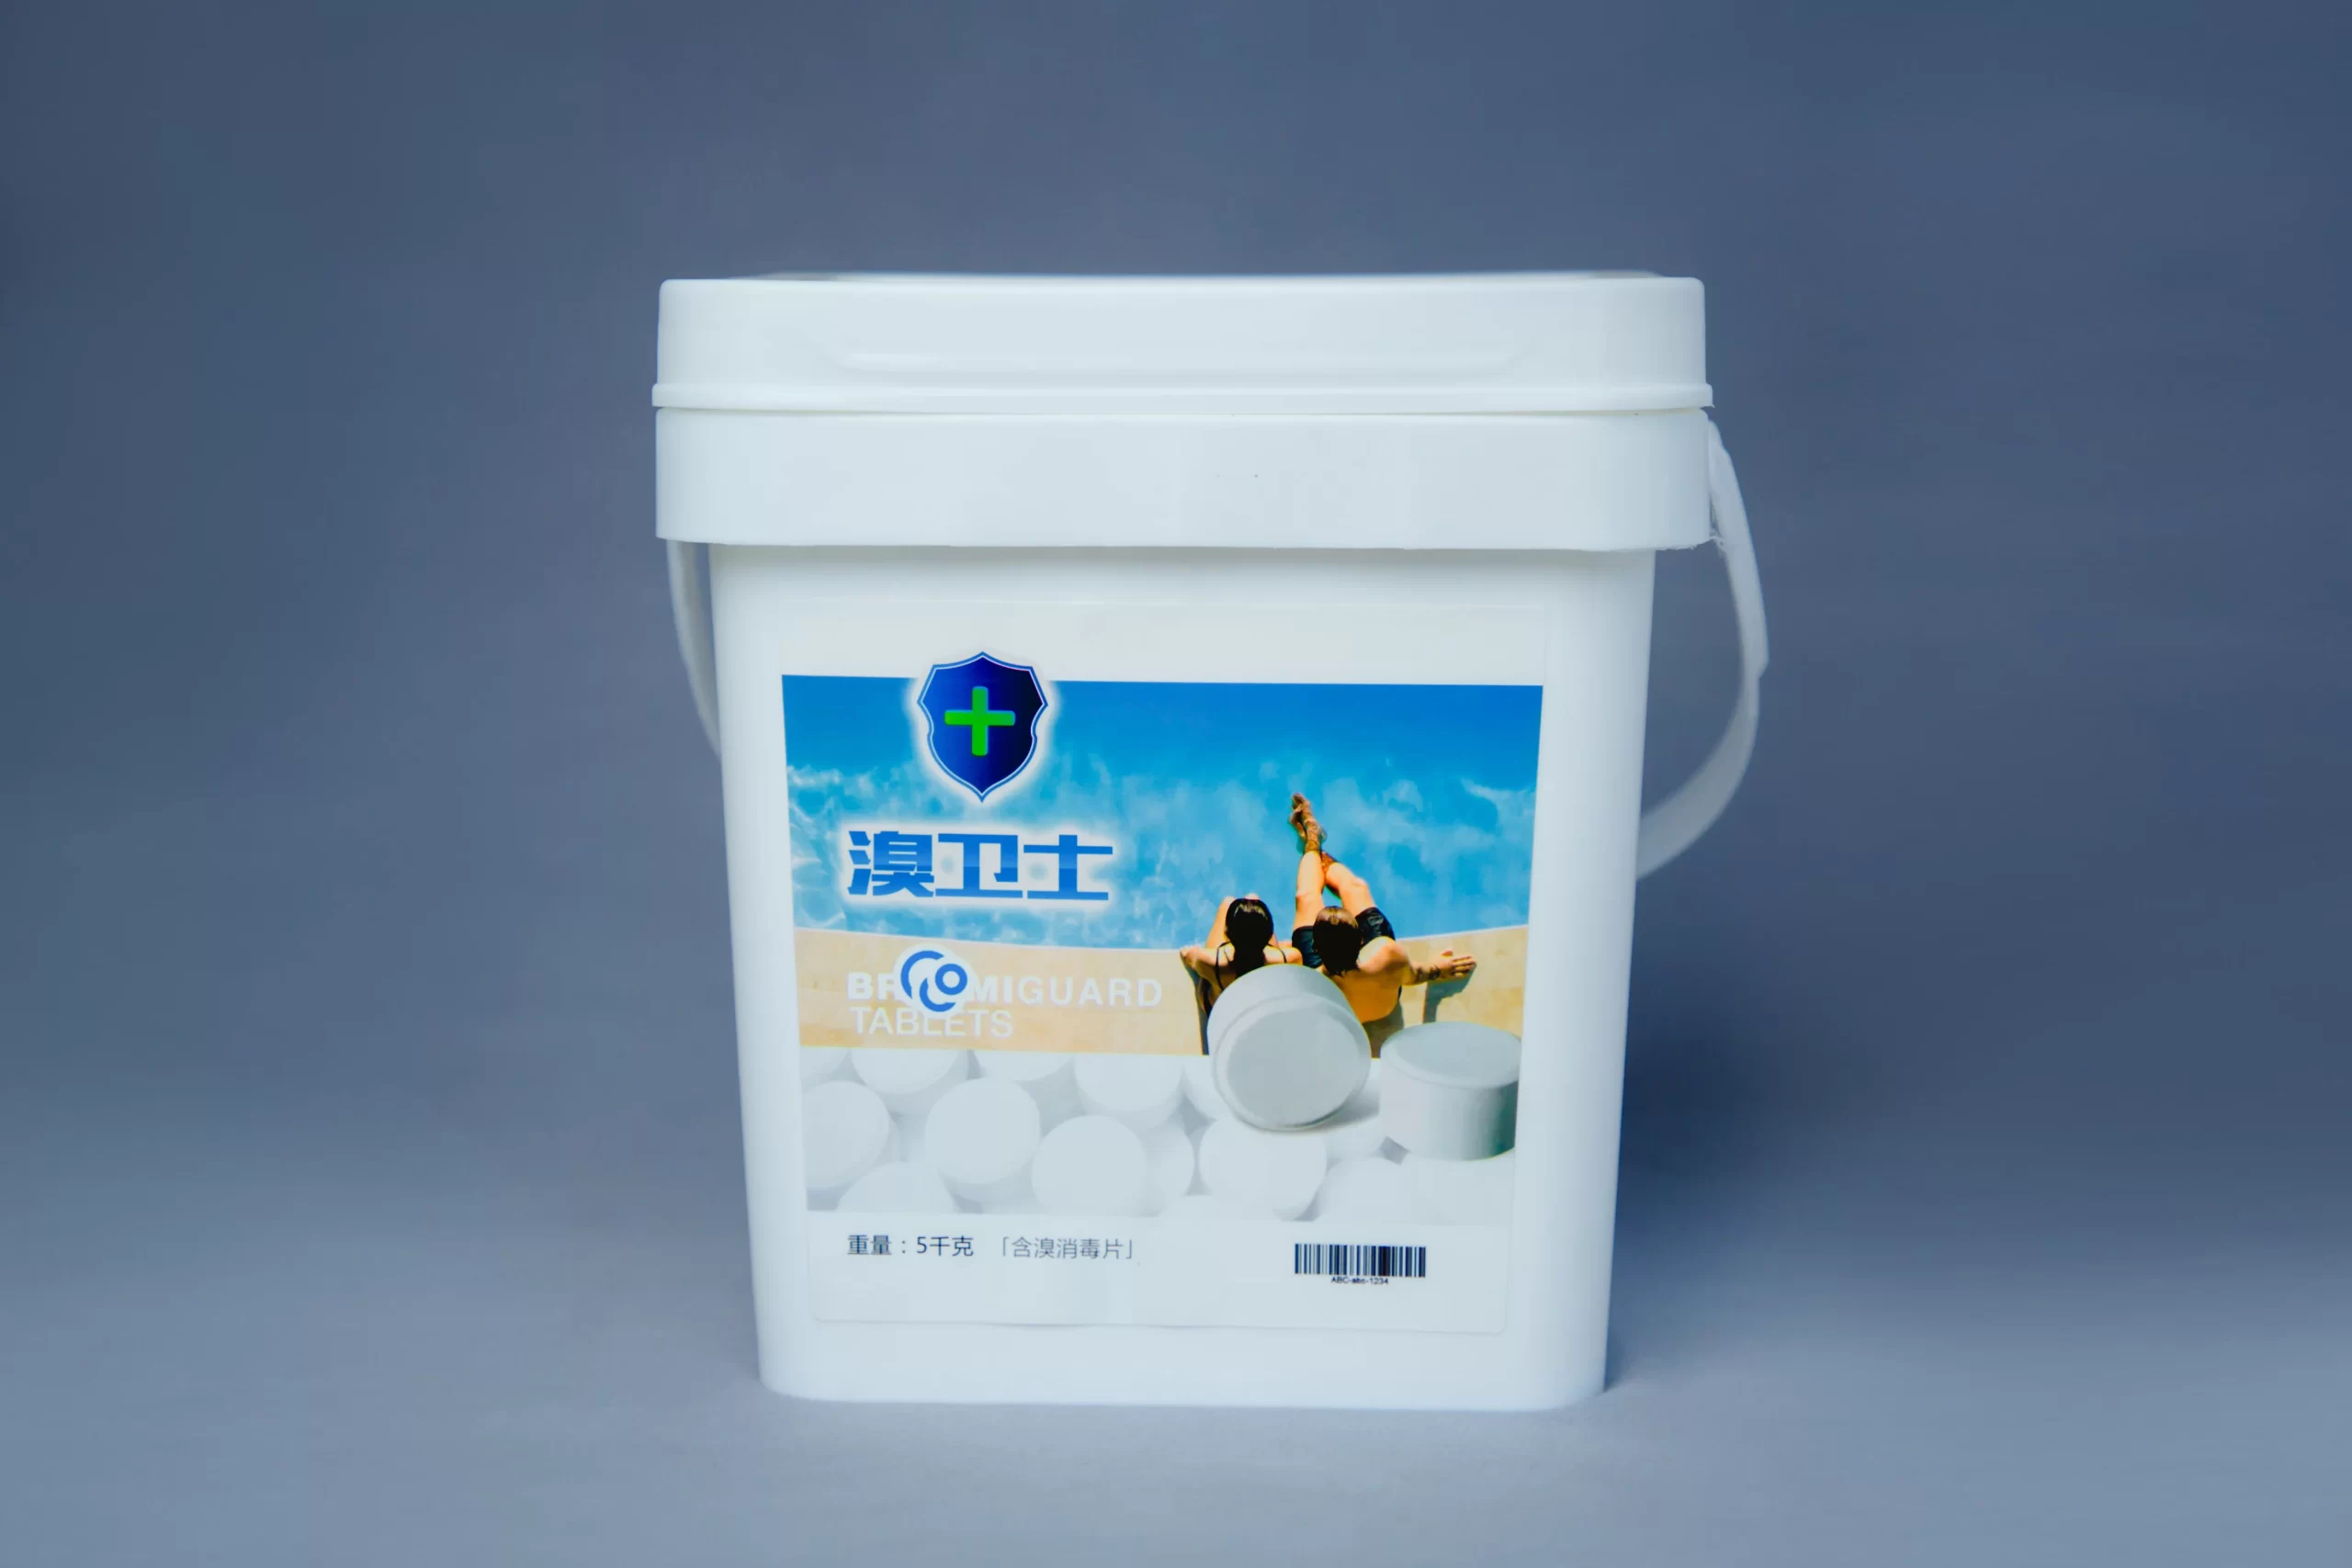
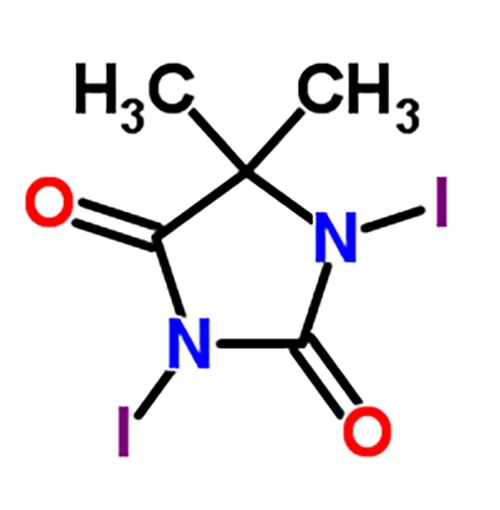
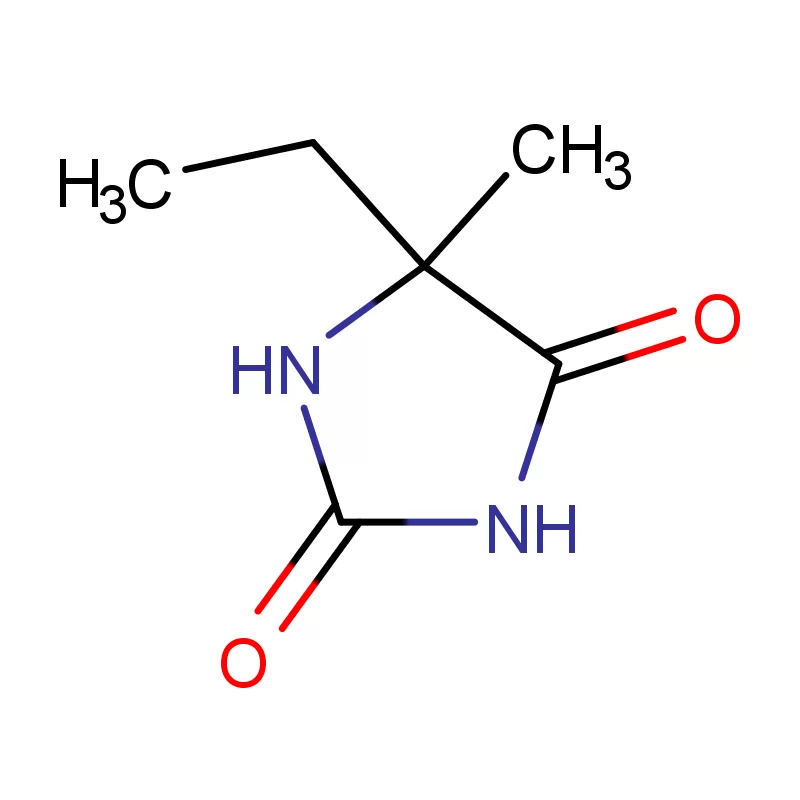
In the realm of chemical formulation, precision is not a luxury; it is a necessity. The efficacy of a sink cleaner tablet relies heavily on the purity of its active ingredients and the consistency of its physical structure. At our manufacturing facility, we move beyond generic production methods by employing state-of-the-art intelligent production lines and digital storage solutions. This ensures that the Bromi Guard Sink Cleaner Tablets factory operations maintain strict control over the synthesis of 5,5-dimethylhydantoin and its derivatives.
Our status as a Hebei Province Level 'A' R&D Institution allows us to continuously refine our formulations, ensuring optimal dissolution rates and cleaning power. The table below outlines how our engineering standards outperform general industry benchmarks, specifically regarding the production of our Bromiguard series.
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Active Ingredient Purity | Determines cleaning and sanitizing power. | High-purity Hydantoin Derivatives (Industrial First Mover) | Superior stain removal and longer shelf-life stability. |
| Production Consistency | Ensures every tablet dissolves and acts identically. | Intelligent Production & Digital Storage | Eliminates batch-to-batch variability common in manual processing. |
| Packaging Precision | Prevents moisture ingress and degradation. | Fully Automatic Packaging Systems | Extended product integrity during global shipping. |
| Regulatory Compliance | Required for market entry in EU/US. | REACH, NSF, BSCI Certified | Seamless customs clearance and market acceptance globally. |
Partnering with a manufacturer that controls the entire value chain—from raw material synthesis to final packaging—is a strategic lever for maximizing Return on Investment (ROI). By sourcing directly from the Bromi Guard Sink Cleaner Tablets factory, businesses eliminate unnecessary intermediaries, ensuring better profit margins and direct access to technical support. Our brands, including Bromiguard and Dr. Brom, have maintained strong sales performance for over 20 years, proving the market longevity and consumer trust inherent in our products.
Furthermore, our location in the Jingjin New Material Industrial Park, combined with our strategic global cooperation network, allows for optimized logistics and reduced lead times. The stability provided by a manufacturer with win-win cooperation in over 50 regions translates to predictable supply chains, allowing our partners to focus on scaling their market presence rather than worrying about stock shortages.
Related products
Top Selling Products