

Email:
info@leachechem.com
In the complex ecosystem of industrial cooling, system efficiency is often compromised by the invisible threats of bio-fouling, scale, and corrosion. Facility managers often face the challenge of balancing potent biocidal efficacy with environmental safety and equipment longevity. Selecting a partner is not merely about procurement; it is about securing the operational integrity of your thermal transfer systems.
Leache Chem Ltd addresses this critical need by bridging the gap between raw chemical manufacturing and sophisticated application. Founded in 1991, we have evolved from a local supplier into a global authority, operating within the Hebei Province Level 'A' R&D Institution framework to deliver solutions that protect your assets.
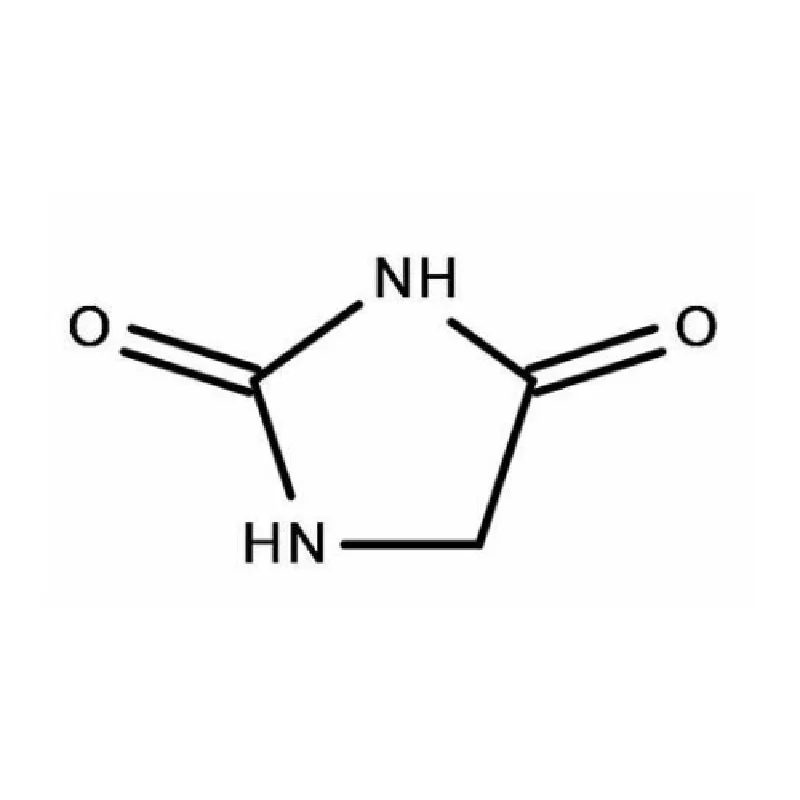
As a dedicated chilled water treatment chemicals manufacturer, we leverage over three decades of expertise to produce high-purity Hydantoin and its derivatives. Our flagship brands, such as 'Bromiguard' and 'Dr. Brom', are trusted in over 50 countries, offering a proven defense against microbial growth that compromises heat exchange efficiency. By integrating intelligent production with NSF-certified safety standards, we ensure that your cooling systems operate at peak performance, minimizing downtime and maintenance costs.
Effective water treatment requires precise chemical engineering. A generic biocide is insufficient for modern high-load cooling systems; stability and purity are paramount. We distinguish ourselves as the first high-tech enterprise in China to realize the industrial production of 5,5-dimethylhydantoin, setting a new benchmark for the industry.
Below is a technical breakdown of how our manufacturing standards translate into tangible advantages for your cooling loop, specifically when evaluating a chilled water treatment chemicals manufacturer.
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Biocidal Stability | Prevents rapid degradation of chemicals in varying pH levels, ensuring consistent microbial control. | Proprietary Hydantoin derivative formulation (Bromiguard™). | Extended half-life in chilled water systems, reducing dosage frequency and chemical consumption. |
| Regulatory Compliance & Safety | Ensures chemicals meet global safety and environmental discharge regulations. | NSF, REACH, and ISO14001 Certified manufacturing processes. | Risk-free compliance for multinational operations, ensuring safety for personnel and the environment. |
| Supply Chain Consistency | Prevents operational stoppages due to chemical unavailability or batch variation. | Intelligent production with digital storage and standardized loading. | Guaranteed batch-to-batch consistency and rapid global logistics from our Economic Development Zone hub. |
| Corrosion Inhibition | Protects expensive chiller metallurgy from chemical attack. | Advanced Thiophene series integration and controlled oxidation. | Preserves equipment lifespan while aggressively eliminating bio-films. |
The true cost of water treatment is not found in the price per drum, but in the total cost of operation (TCO) involving energy consumption and asset lifecycle. Partnering with a scientifically advanced chilled water treatment chemicals manufacturer allows you to shift from reactive maintenance to predictive value engineering.
Leache Chem Ltd empowers this shift through "Win-Win" strategic cooperation. By utilizing our advanced derivatives, facilities can maintain cleaner heat transfer surfaces (films), which directly correlates to reduced electrical load on chillers. Furthermore, our robust production capacity (supported by 101-250 specialized staff) and independent brand reliability mean you are insulated from market volatility. The chart below illustrates the projected efficiency retention when utilizing high-grade hydantoin-based treatment versus generic alternatives over a 5-year equipment cycle.
Related products
Top Selling Products