Email:
info@leachechem.com

Managing the delicate balance of closed-loop cooling systems is a constant battle against corrosion, scaling, and biological fouling. We understand that for facility managers and industrial engineers, the primary goal is operational continuity without the headache of unexpected shutdowns. As a premier chilled water treatment chemicals supplier, Leache Chem Ltd does not just sell additives; we provide the chemical assurance needed to maintain peak thermal transfer efficiency.
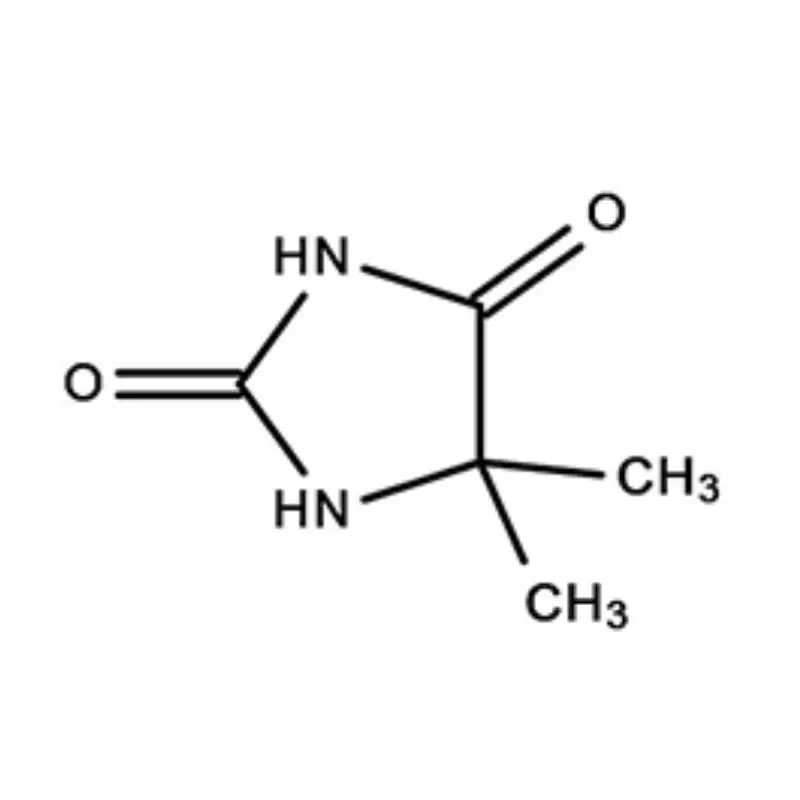
Established in 1991, our expertise goes beyond basic mixing. We are the first high-tech enterprise in China to realize the industrial production of 5,5-dimethylhydantoin and its derivatives—core components in high-efficacy biocides like our Bromiguard and Dr. Brom series. With NSF and ISO certifications backing our production in Hebei, we offer a level of purity and regulatory compliance that generic suppliers cannot match. When you choose us as your chilled water treatment chemicals supplier, you are leveraging over three decades of R&D focused on protecting your infrastructure and extending the lifecycle of your cooling assets across more than 50 countries.
In the realm of industrial cooling, chemical consistency is synonymous with system safety. Variable quality in biocide formulation can lead to resistant bacterial strains and biofilm accumulation, drastically reducing heat exchange rates. Leache Chem Ltd distinguishes itself as a chilled water treatment chemicals supplier through intelligent production lines and digital storage solutions that eliminate human error.
Our facility, recognized as a Hebei Province Level 'A' R&D Institution, adheres to strict international protocols. We utilize advanced hydantoin synthesis to create stable, broad-spectrum control agents. The following table outlines how our manufacturing standards translate into tangible performance benefits for your chilled water systems compared to general industry benchmarks.
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Chemical Purity & Stability | Determines dosage efficiency and reduced sludge buildup. | Automated synthesis of 5,5-dimethylhydantoin (Pioneer in China). | Higher active content requiring lower dosage volumes. |
| Regulatory Compliance | Essential for safety audits and environmental discharge. | Full certification suite: ISO9001, ISO14001, REACH, NSF International. | Risk-free compliance for global supply chains. |
| Supply Chain Resilience | Prevents stockouts during critical cooling seasons. | Intelligent production with digital storage & standardized loading. | Guaranteed availability for 50+ export regions. |
| Bio-fouling Control | Prevents Legionella and slime affecting heat transfer. | Proprietary brands (Bromiguard, Dr. Brom) with 20+ year track record. | Proven eradication of resistant biological films. |
Selecting a vendor is a financial strategy, not just a procurement task. Working with a scientifically advanced chilled water treatment chemicals supplier shifts the focus from the cost-per-drum to the cost-per-year of system operation. Inefficient treatment leads to microscopic scaling, where even 0.8mm of scale can increase energy consumption by nearly 10%.
Leache Chem Ltd empowers clients to optimize their Total Cost of Ownership (TCO). By utilizing our premium derivatives and "Bromiguard" solutions, facilities prevent the compounding energy costs associated with fouled heat exchangers. The chart below illustrates the projected retention of Heat Transfer Efficiency (HTE) when utilizing high-purity, stable chemical treatment versus generic alternatives over an operational year.
Related products
Top Selling Products