

Email:
info@leachechem.com
In the competitive landscape of water treatment and chemical additives, sourcing managers often face the dual challenge of ensuring supply chain stability while maintaining rigorous purity standards. Finding a partner who can balance industrial scale with precise chemical engineering is difficult, especially when navigating global regulations. Since 1991, Leache Chem Ltd has emerged as a stabilizing force in the chemical industry, addressing these exact pain points through decades of operational excellence.
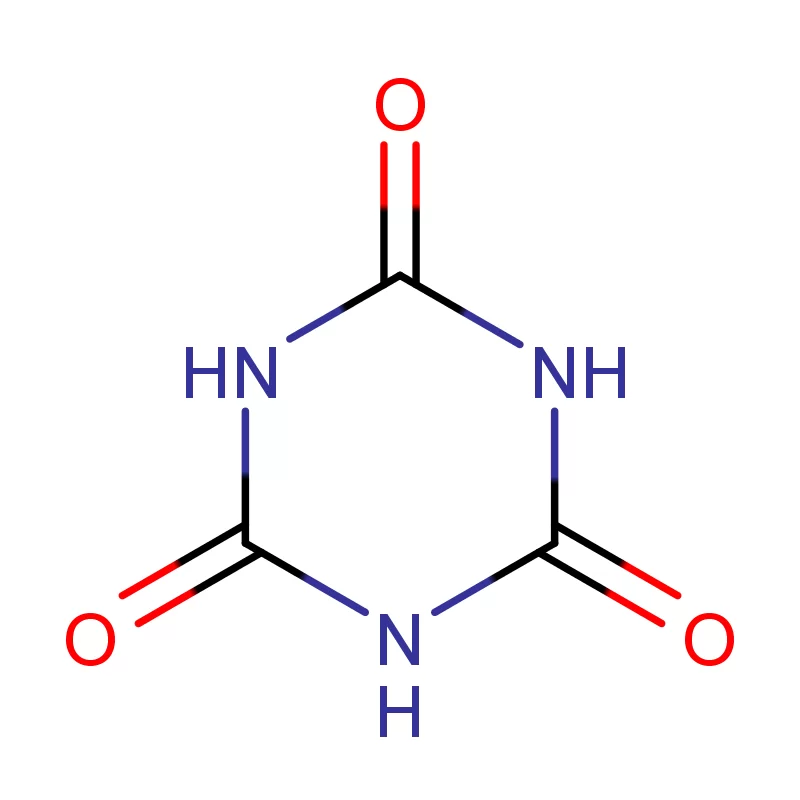
We understand that reliable chemical sourcing is not just about the product; it is about the assurance of continuity. As a recognized Cyanuric Acid manufacturer with a global footprint, we leverage our status as a Hebei Province Level 'A' R&D Institution to deliver consistent quality. Our facility, located in the Jingjin New Material Industrial Park, integrates intelligent production systems that mitigate human error and ensure every batch meets international compliance. By holding authoritative certifications such as NSF, REACH, and ISO9001, we provide our partners in over 50 countries with the confidence that their supply chain is secure, compliant, and optimized for performance.
Technical superiority in chemical manufacturing is defined by the convergence of automation, quality control, and environmental stewardship. For a Cyanuric Acid manufacturer, the ability to control particle size, moisture content, and chemical stability is paramount. At Leache Chem, we have moved beyond traditional manufacturing methods. We employ a fully digitized workflow—from intelligent production lines to automatic packaging and digital storage—ensuring that our output maintains the highest integrity from reactor to delivery.
Our commitment to being a high-tech enterprise is validated by our ability to meet stringent international standards. Below is a breakdown of how our engineering protocols translate into tangible technical advantages for your applications:
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Regulatory Compliance | Ensures market access in EU and US markets. | Full REACH Registration & NSF Certification | Eliminates legal bottlenecks and guarantees safety for end-users. |
| Process Consistency | Prevents batch-to-batch variation affecting formulations. | Intelligent Production & Digital Storage Systems | Zero-defect stability enabling precise downstream formulation. |
| Environmental Safety | Critical for sustainable supply chain audits. | ISO14001 & OHSAS18001 Accredited Systems | Reduces carbon footprint and ensures long-term factory viability. |
| R&D Responsiveness | Adaptability to new chemical requirements. | Level 'A' R&D Institution Status | Rapid customization of chemical properties to meet specific client needs. |
True value in chemical procurement extends far beyond the price per metric ton. It encompasses the reduction of risk, the longevity of supplier relationships, and the efficiency of logistics. Partnering with a strategic Cyanuric Acid manufacturer like Leache Chem allows businesses to unlock hidden ROI through streamlined operations. Our established brands, including 'Bromiguard' and 'Dr. Brom', have demonstrated market resilience for over 20 years, proving that quality inputs lead to superior end-products and stronger brand loyalty for our clients.
By establishing deep, win-win cooperation with us, companies mitigate the hidden costs associated with delayed shipments or non-compliant materials. Our automated packaging and standardized loading procedures minimize logistics losses, while our massive capacity (supported by 101-250 staff) ensures scalability. The chart below illustrates the efficiency gains and customer retention stability our partners experience when integrating our standardized supply chain solutions.
Related products
Top Selling Products