Email:
info@leachechem.com

In the volatile landscape of chemical sourcing, finding a stable supply partner is often the most significant challenge for procurement managers. Fluctuations in raw material purity and inconsistent production schedules can disrupt downstream applications, particularly in water treatment and sanitation sectors. Securing a partnership with a proven DBDMH factory is not just about purchasing a commodity; it is about establishing a lifeline for your supply chain.
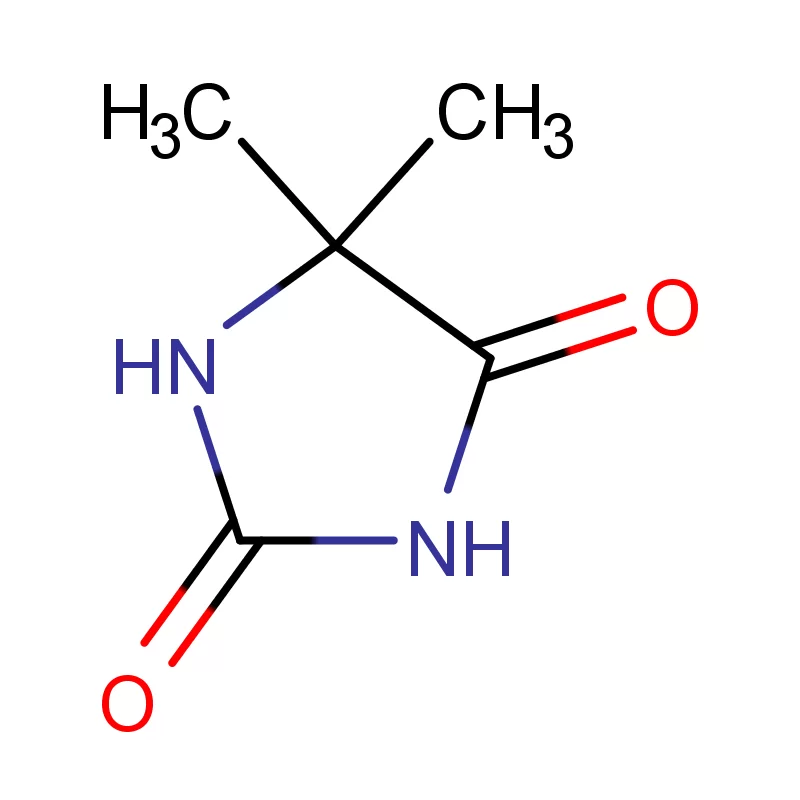
Leache Chem Ltd addresses these challenges by leveraging over three decades of manufacturing heritage. Established in 1991, we stand as a pioneer in the industry, distinguished as the first high-tech enterprise in China to achieve industrial production of 5,5-dimethylhydantoin and its derivatives. By controlling the core precursor chemistry, our facility ensures that every batch leaving our DBDMH factory meets rigorous global standards. Our location within the Jingjin New Material Industrial Park allows us to integrate intelligent production with digital storage, providing our partners with the certainty they need in an uncertain market.
Consistency in biocide manufacturing requires more than just capacity; it demands a rigorous adherence to international engineering and regulatory protocols. At Leache Chem, our status as a Hebei Province Level 'A' R&D Institution drives the technical superiority of our output. We employ intelligent production systems and standardized loading procedures to eliminate human error, ensuring that our output remains the industry benchmark.
The following table illustrates how the operational standards of our DBDMH factory translate into tangible technical advantages for our global clientele.
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Regulatory Compliance | Critical for market entry in EU and US markets. | Comprehensive portfolio: REACH, ISO9001, NSF, BSCI. | Zero-friction customs clearance and immediate regulatory approval. |
| Production Consistency | Ensures stable dosing in end-user applications. | Intelligent production with automated packaging lines. | Uniform particle size and chemical stability across all batches. |
| Supply Chain Resilience | Prevents stockouts during global shortages. | Digital storage systems & Scale (101-250 employees). | Real-time inventory visibility and guaranteed lead times. |
| Environmental Safety | Reduces liability and aligns with ESG goals. | ISO14001 & OHSAS18001 Certified facility. | Sustainable sourcing partner that lowers reputational risk. |
Choosing the right manufacturing partner is a strategic financial decision. Working directly with a manufacturer that possesses deep vertical integration—from the hydantoin precursor to the final brominated derivative—eliminates unneccessary intermediaries and cost layers. Our established independent brands, including 'Bromiguard' and 'Dr. Brom', demonstrate a twenty-year track record of market acceptance, proving that products from our DBDMH factory deliver lasting value.
By leveraging our strategic presence in over 50 countries, clients benefit from economies of scale and a "win-win" cooperation model. The chart below visualizes the efficiency gains and risk reduction achieved by partnering with a fully certified, intelligent manufacturing hub compared to conventional sourcing methods.
Related products
Top Selling Products