Email:
info@leachechem.com

Sourcing high-efficacy biocides and water treatment chemicals often presents a complex challenge: balancing purity requirements with supply chain reliability. For industries reliant on precise halogen stabilization, the volatility of raw materials can disrupt production schedules and compromise end-product quality. Identifying a partner who controls the entire synthesis value chain—from precursor manufacturing to final halogenation—is critical for mitigating these risks.
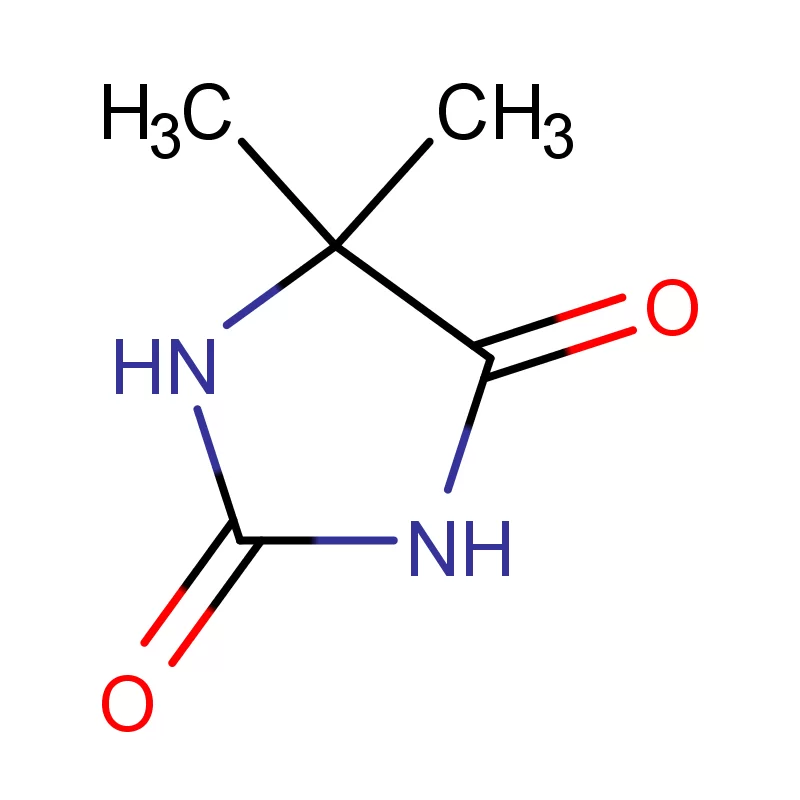
Leache Chem Ltd eliminates these uncertainties by operating as a vertically integrated powerhouse in the hydantoin sector. Established in 1991, we were the first high-tech enterprise in China to realize the industrial production of 5,5-dimethylhydantoin (DMH), the essential backbone for creating premium DBDMH. By securing the core chemistry, we provide our partners with a stable, scalable supply that market traders simply cannot match.
With a footprint spanning over 50 countries and a facility located in the Jingjin New Material Industrial Park, our infrastructure is built to withstand global demand fluctuations. When you collaborate with a DBDMH manufacturer that owns its intellectual property and production lines—evidenced by our Level 'A' R&D Institution status in Hebei Province—you secure more than just a chemical product; you secure operational continuity.
In the specialized field of halogenated hydantoins, technical consistency is the primary differentiator between a generic commodity and a performance chemical. A top-tier DBDMH manufacturer must adhere to rigorous engineering protocols to ensure that the release of bromine and chlorine remains controlled and predictable in application. Our approach leverages intelligent production systems and digital storage to minimize human error and environmental contamination.
Through brands like "Bromiguard" and "Dr. Brom," which have maintained market dominance for over 20 years, we demonstrate that strict adherence to ISO and NSF standards translates directly to product efficacy. Below is an analysis of how our engineering standards outperform general industry benchmarks.
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Regulatory Compliance | Ensures market access (EU/USA) and safety. | Comprehensive portfolio: REACH, NSF, ISO9001, ISO14001, OHSAS18001. | Zero barriers to entry in regulated markets; guaranteed environmental safety. |
| Production Consistency | Determines lot-to-lot chemical uniformity. | Intelligent production lines with standardized loading and digital storage. | Eliminates batch variance, ensuring predictable dosing for end-users. |
| R&D Capability | Capacity to customize and refine derivatives. | Recognized Hebei Province Level 'A' R&D Institution. | Ability to adapt formulations for specific oxidizing requirements. |
| Supply Chain Integrity | Prevents contamination and delays. | Automatic packaging and location in a specialized New Material Industrial Park. | Maintains high purity during transit; robust logistics infrastructure. |
True value in chemical procurement is not defined solely by the price per metric ton, but by the reduction of total cost of ownership (TCO) through compliance and efficiency. Partnering with a fully certified DBDMH manufacturer like Leache Chem allows businesses to bypass the expensive hurdles of regulatory validation. Our possession of BSCI and NSF certifications means our clients face fewer audits, lower compliance risks, and faster time-to-market for their end products.
Furthermore, our standardized automated packaging reduces product loss and handling time, directly improving your bottom line. The chart below illustrates the comparative advantage in long-term operational efficiency when choosing a manufacturer with integrated R&D and intelligent production versus standard market suppliers.
Related products
Top Selling Products