Email:
info@leachechem.com

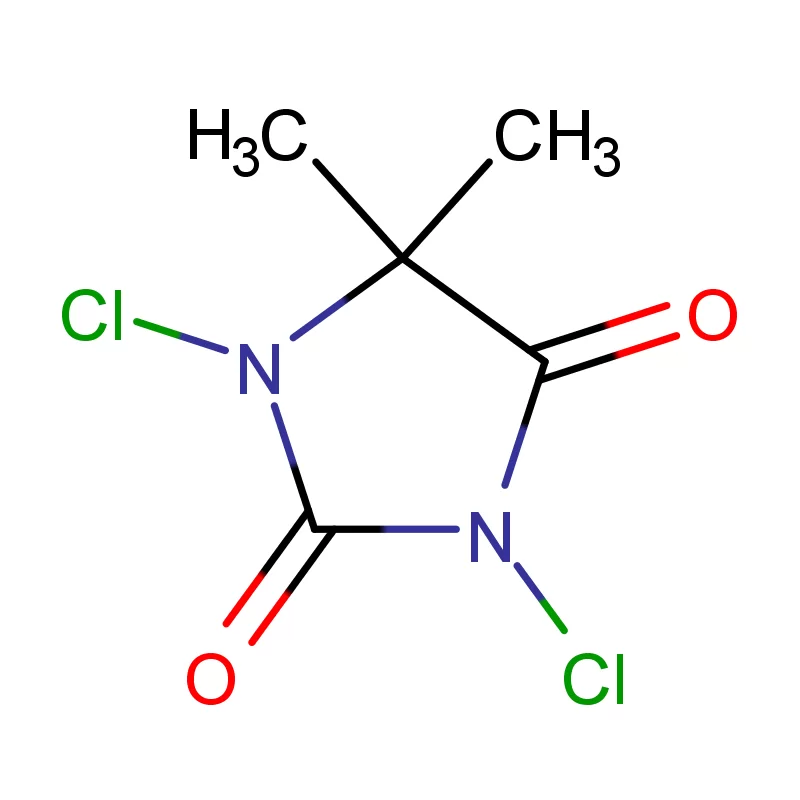
In the competitive landscape of water treatment and industrial disinfection, sourcing a reliable DCDMH product is often complicated by supply chain volatility and inconsistent chemical purity. Manufacturers and procurement officers frequently face the challenge of balancing cost-efficiency with the rigorous safety standards required for global export. The stakes are high; a compromise in chemical stability can lead to operational downtime or regulatory non-compliance in critical markets.
Leache Chem Ltd addresses this challenge by leveraging over three decades of specialized experience. Founded in 1991, we are the first high-tech enterprise in China to realize the industrial production of 5,5-dimethylhydantoin and its derivatives. This foundational expertise ensures that when you select our DCDMH product, you are backing your operations with a supply chain that currently supports hundreds of partners across more than 50 countries.
We move beyond simple transaction-based relationships. By operating from the Jingjin New Material Industrial Park with intelligent production capabilities, we solve the common industry pain point of batch-to-batch variation. Our approach transforms the procurement of hydantoin derivatives from a logistical hurdle into a strategic advantage, ensuring your downstream applications receive high-performance chemical inputs every time.
The efficacy of a halogenated hydantoin depends entirely on the precision of its manufacturing process. At Leache Chem, we do not merely produce chemicals; we engineer stability. As a Hebei Province Level 'A' R&D Institution, we enforce strict protocols that govern the synthesis of our DCDMH product. Our facility integrates intelligent production lines with standardized loading procedures, eliminating the human error often associated with manual chemical handling.
To demonstrate our commitment to quality, we benchmark our production against the highest international requirements. The table below outlines how our technical infrastructure translates into tangible performance metrics for your applications.
| Performance Metric | Industry Significance | Our Engineering Standard | Client Advantage |
|---|---|---|---|
| Regulatory Compliance | Critical for market entry in EU and US sectors. | NSF, REACH & ISO Certifications (9001/14001) | Ensures your DCDMH product meets global safety and environmental mandates without legal friction. |
| Purity Consistency | Prevents dosage fluctuations in water treatment. | Intelligent Production Systems | Automated synthesis reduces impurities, maximizing the active halogen content. |
| Supply Chain Security | Mitigates risk of stockouts during peak demand. | Digital Storage & Automatic Packaging | Real-time inventory tracking ensures on-time delivery for high-volume orders. |
| Workplace Safety | Reduces liability and contamination risks. | OHSAS18001 Standards | Sustainable production of DCDMH product derivatives protects both workers and the end product. |
By adhering to these rigorous standards, Leache Chem ensures that our independent brands, including 'Bromiguard' and 'Dr. Brom', maintain their reputation for excellence which has been established over 20 years of market presence.
True value in chemical procurement is measured not just by the price per metric ton, but by the long-term reliability of the solution. Investing in a premium DCDMH product from a manufacturer with full-scale industrial control yields a higher Return on Investment (ROI) by minimizing waste and preventing system corrosion caused by inferior by-products. Leache Chem's integrated approach—spanning R&D to digital storage—allows clients to optimize their chemical usage rates.
Our strategic positioning in the Jingjin New Material Industrial Park allows us to scale production efficiently, passing cost benefits to our partners without compromising on the specifications of the DCDMH product. With a history of deep, win-win cooperation with global clients, we empower you to forecast costs accurately and secure your supply chain against market volatility.
Related products
Top Selling Products