Email:
info@leachechem.com

In the highly regulated world of chemical disinfection, sourcing reliability is often the primary bottleneck for global buyers. You are likely seeking a manufacturing partner that not only guarantees efficacy but also ensures compliance across international borders. The challenge lies in finding a facility that balances high-volume capacity with the rigorous quality control required for independent brands like Dr. Brom.
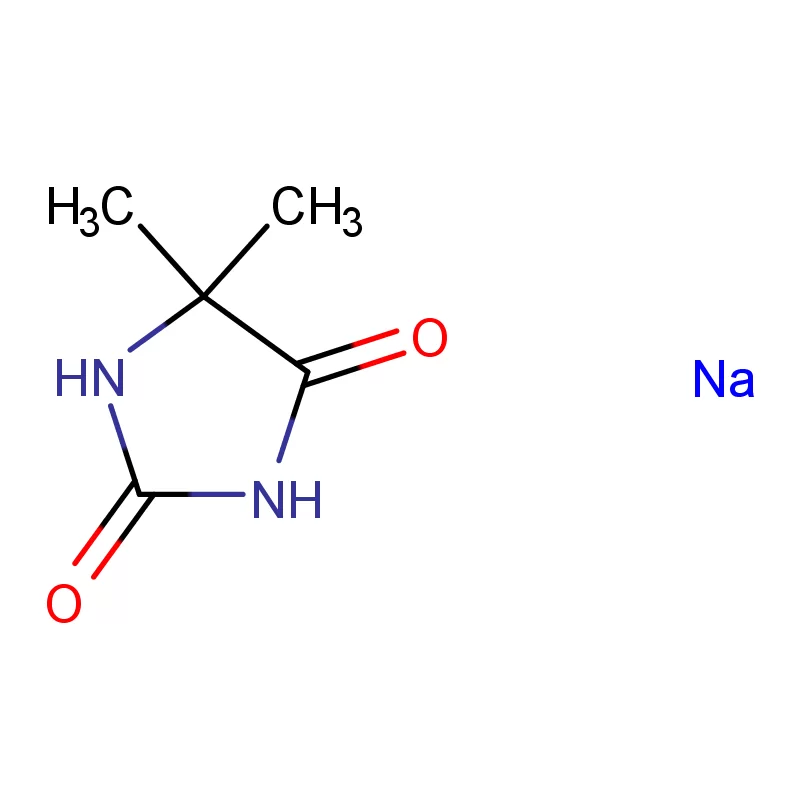
Leache Chem Ltd, established in 1991, addresses these pain points by offering a fully integrated solution. As a world-class leading professional manufacturer of hydantoin and its derivatives, we operate beyond the scope of a standard assembly line. Our facility is the first high-tech enterprise in China to realize the industrial production of 5,5-dimethylhydantoin—the core precursor for high-quality bromine disinfection.
By locating our operations in the Jingjin New Material Industrial Park and securing ISO9001, ISO14001, and NSF certifications, we provide the assurance you need. When you choose our Dr Bromine Disinfection Effervescent Tablets factory, you are accessing a legacy of over 20 years of market success, backed by a supply chain that serves customers in more than 50 countries.
Consistency in effervescent technology requires precision engineering. A fluctuation in moisture control or compression pressure can lead to tablets that dissolve prematurely or fail to meet active ingredient standards. At Leache Chem, we have transitioned from traditional manufacturing to a model of intelligent production. Our facility, recognized as a Hebei Province Level 'A' R & D Institution, employs automated packaging and digital storage systems to eliminate human error.
We believe that a premium Dr Bromine Disinfection Effervescent Tablets factory must adhere to metrics that exceed basic industry requirements. Below is a breakdown of our technical performance standards compared to general market expectations:
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Active Content Stability | Determines shelf-life and efficacy. | Vertical integration of Hydantoin precursors. | Higher purity and longer shelf-life for 'Bromiguard' & 'Dr. Brom' series. |
| Production Consistency | Reduces batch-to-batch variance. | Intelligent Production & ISO9001 Protocols. | Uniform tablet weight and dissolution rates. |
| Regulatory Compliance | Market access (US, EU, etc.). | NSF, REACH, BSCI, OHSAS18001. | Seamless export capabilities to 50+ countries. |
| Packaging Integrity | Moisture protection. | Fully Automatic Packaging Lines. | Zero-contact packaging minimizes contamination risks. |
In the chemical commodity market, price is often conflated with value. However, true Return on Investment (ROI) is derived from supply chain resilience and brand protection. Partnering with Leache Chem allows you to leverage our "Strategic Win-Win" philosophy. Because we control the production of key derivatives like 5,5-dimethylhydantoin, we insulate our partners from the volatile fluctuations of raw material costs that plague smaller, assembly-only factories.
Our status as a trusted Dr Bromine Disinfection Effervescent Tablets factory is not just about manufacturing; it is about brand acceleration. With established independent brands like 'Leache' and 'Dr. Brom' having sold well for decades, we transfer this manufacturing expertise to your private label needs. This results in reduced defect rates and faster speed-to-market.
The chart below illustrates the efficiency gains in lead time and quality consistency experienced by our partners over a 5-year cooperation cycle compared to industry averages.
Related products
Top Selling Products