Email:
info@leachechem.com

Sourcing high-purity chemical precursors often involves navigating a maze of regulatory hurdles, inconsistent purity levels, and supply chain volatility. For pharmaceutical manufacturers, the risk of a delayed shipment or a batch failing quality control is not just a financial loss; it is a disruption to vital healthcare solutions. Finding a partner who understands the intricate balance between industrial capacity and pharmaceutical-grade compliance is the primary challenge facing procurement teams today.
Since 1991, Leache Chem Ltd has emerged as a definitive answer to these sourcing complexities. By combining the capabilities of a Hebei Province Level 'A' R&D Institution with a global export network, we bridge the gap between raw chemical manufacturing and specific pharmaceutical needs. Our history of serving hundreds of customers across more than 50 countries proves that stability is achievable. As a dedicated drug intermediates exporter, we leverage intelligent production systems and digital storage solutions to ensure that your supply chain remains robust, transparent, and strictly aligned with global standards like REACH and NSF.
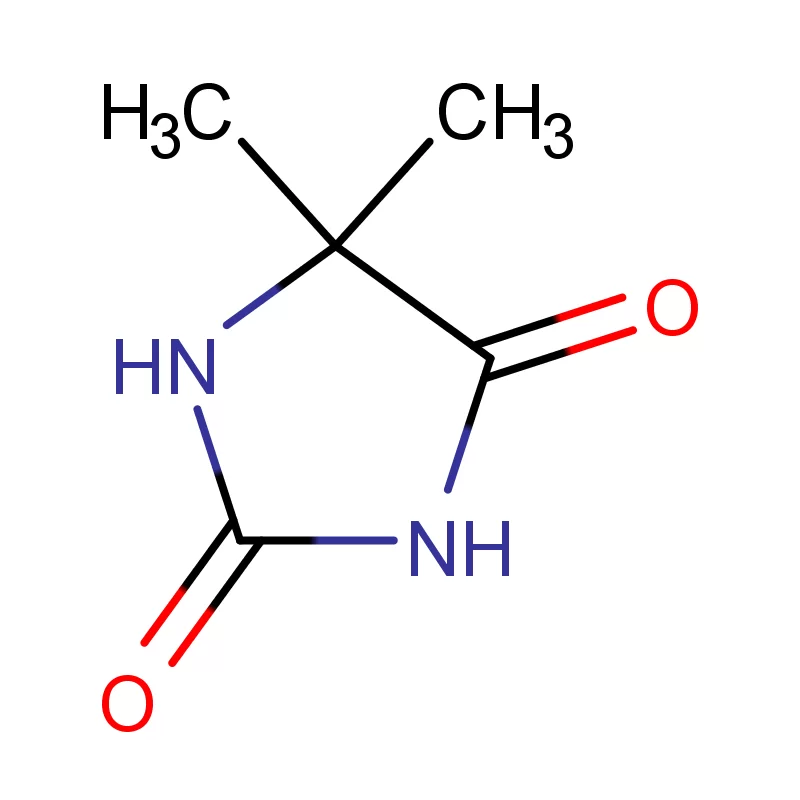
In the realm of intermediate synthesis, technical precision is non-negotiable. Merely meeting basic specifications is insufficient for modern pharmaceutical applications; the manufacturing process must demonstrate repeatability, traceability, and advanced process control. Leache Chem Ltd stands as the first high-tech enterprise in China to realize the industrial production of 5,5-dimethylhydantoin and its derivatives, setting a benchmark for the industry.
Our facility, located in the Jingjin New Material Industrial Park, operates under a philosophy of intelligent automation. From automatic packaging to standardized loading, every step is optimized to minimize human error and contamination risks. The following table outlines how our technical parameters translate into tangible advantages for clients seeking a qualified drug intermediates exporter.
| Performance Metric | Industry Significance | Our Engineering Standard | Client Advantage |
|---|---|---|---|
| Regulatory Compliance | Ensures market access and safety. | ISO9001, ISO14001, OHSAS18001, REACH, BSCI, NSF Certifications. | Seamless entry into EU and US markets with reduced auditing friction. |
| Synthesis Capability | Determines product purity and volume. | World-class Hydantoin & Thiophene series production; First in China for 5,5-dimethylhydantoin. | Access to proprietary, high-purity synthesis routes unavailable elsewhere. |
| Logistics Precision | Prevents degradation and delay. | Digital storage systems and standardized loading protocols. | Guaranteed material integrity upon arrival, regardless of global destination. |
| R&D Innovation | Future-proofs product supply. | Recognized Hebei Province Level 'A' R&D Institution. | Rapid adaptation to new custom synthesis requirements and formula adjustments. |
Selecting a supplier is a strategic investment decision that impacts your bottom line far beyond the initial purchase price. A transactional approach to sourcing often leads to hidden costs associated with compliance failures or production downtime. By partnering with Leache Chem Ltd, organizations unlock a value-engineered supply chain. Our long-term, win-win cooperation model, validated by over 20 years of market presence with independent brands like 'Bromiguard' and 'Dr. Brom', ensures that your procurement strategy contributes to sustainable growth.
We transform the role of a drug intermediates exporter from a vendor to a strategic asset. Our intelligent production capabilities reduce waste and overhead, savings which are passed down to our partners. Furthermore, our comprehensive certification portfolio (ISO, NSF, REACH) eliminates the expensive need for third-party remedial testing or regulatory fines. The chart below illustrates the comparative value drivers when engaging with our advanced manufacturing ecosystem.
Related products
Top Selling Products