Email:
info@leachechem.com

In the pharmaceutical and chemical synthesis sectors, sourcing reliability is often the biggest bottleneck. Finding a partner who can balance scalability with stringent regulatory compliance is a challenge that keeps procurement managers awake at night. When supply chains fracture or purity levels fluctuate, the downstream costs can be astronomical. We understand that you require more than just a vendor; you need a manufacturing partner capable of navigating complex regulatory landscapes while delivering consistent quality.
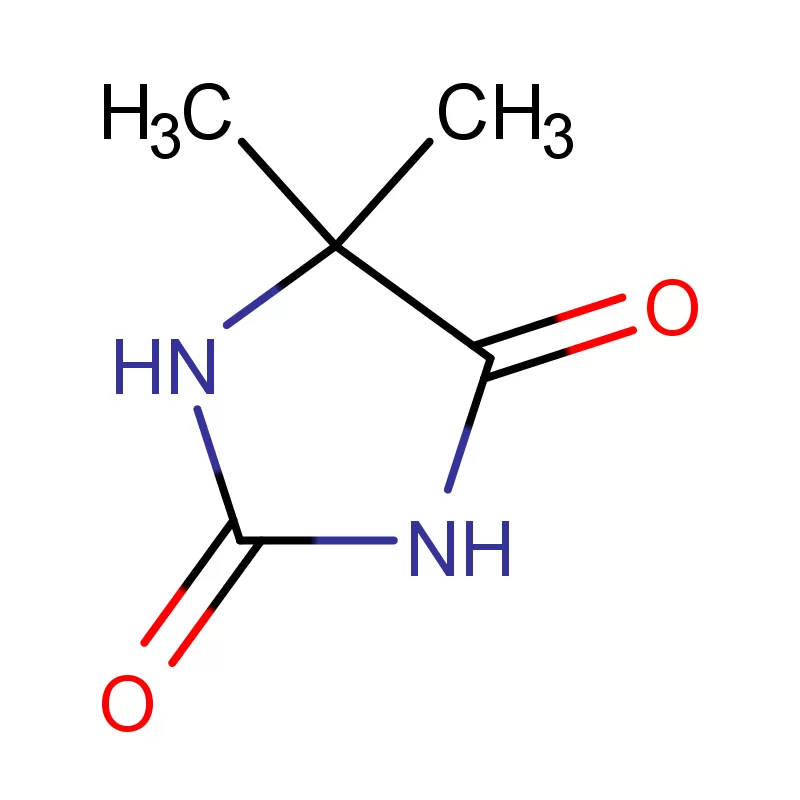
Leache Chem Ltd eliminates these uncertainties by operating as a premier drug intermediates factory with a legacy dating back to 1991. As a Hebei Province Level 'A' R&D Institution, we bridge the gap between laboratory innovation and industrial-scale execution. Unlike generic suppliers, we have pioneered the industrial production of specialized derivatives, such as 5,5-dimethylhydantoin, in China. With a footprint expanding across 50+ countries and certifications including ISO9001, REACH, and NSF, we provide the assurance needed to secure your production lines against volatility.
Operational excellence in chemical manufacturing is defined by the integration of automation and rigorous quality control. A modern drug intermediates factory must move beyond manual processes to ensure batch-to-batch consistency. At our facility located in the Jingjin New Material Industrial Park, we employ intelligent production systems that govern everything from synthesis to digital storage.
Our technical infrastructure is designed to meet the exacting standards of international pharmacopeias and industrial applications. By utilizing independent brands like 'Bromiguard' and 'Dr. Brom', we demonstrate a commitment to proprietary quality control that generic manufacturers cannot match. Below is an analysis of how our engineering standards translate into tangible advantages for your supply chain.
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Process Control & Purity | Critical for downstream reaction yield and drug safety. | Intelligent production lines with real-time digital monitoring. | Minimizes human error, ensuring 99%+ purity consistency. |
| Regulatory Compliance | Mandatory for market access in EU and US markets. | Full certification suite: ISO9001, ISO14001, REACH, NSF, BSCI. | Seamless customs clearance and audit readiness for global clients. |
| Production Scalability | Ability to handle fluctuating market demands. | Industrial-scale capacity for Hydantoin/Thiophene series (First in China for specific derivatives). | Guaranteed volume availability without lead-time penalties. |
| Logistics Integrity | Prevents contamination and degradation during transit. | Automatic packaging coupled with standardized loading protocols. | Zero contamination risk during transport to 50+ countries. |
Selecting the right manufacturing partner is a strategic financial decision. Working with a scientifically advanced drug intermediates factory allows you to transition from transactional purchasing to value engineering. By leveraging our established history since 1991, clients avoid the hidden costs associated with re-validation, rejected batches, and supply interruptions.
Our philosophy is built on "win-win" cooperation. We do not simply sell chemicals; we optimize your procurement strategy. Through our digital storage and automated logistics, we reduce inventory holding costs and streamline just-in-time delivery. The chart below illustrates the comparative advantage of partnering with a certified, intelligent manufacturer versus a standard supplier regarding operational efficiency and risk reduction over time.
Related products
Top Selling Products