Email:
info@leachechem.com

In the highly regulated pharmaceutical landscape, sourcing instability and inconsistent purity profiles are critical bottlenecks that can derail entire production timelines. For procurement officers and supply chain managers, the challenge lies not just in finding a supplier, but in securing a partner capable of navigating complex regulatory environments while maintaining industrial scalability. A reliable drug substance intermediate factory must transcend basic manufacturing to offer a synchronized ecosystem of quality assurance and logistical precision.
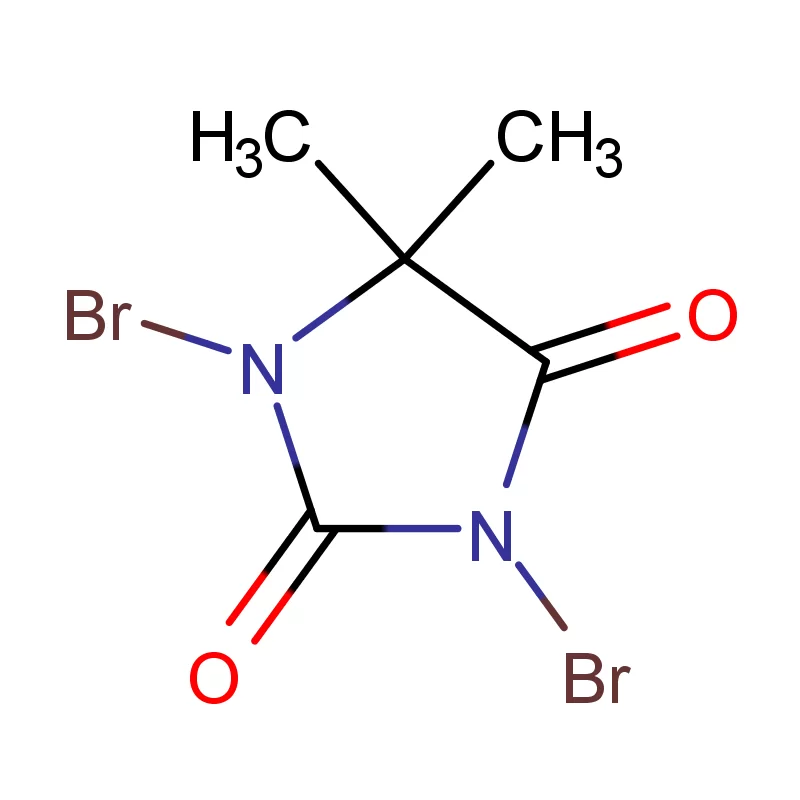
Since 1991, Leache Chem Ltd has engineered a solution to these supply chain vulnerabilities. As a recognized Hebei Province Level 'A' R&D Institution, we do not merely manufacture chemicals; we solve the continuity problems faced by global pharmaceutical entities. By integrating intelligent production systems with a legacy of innovation—including being the first in China to realize industrial production of 5,5-dimethylhydantoin—we provide the stability required for high-stakes pharmaceutical formulation. With a footprint expanding across 50 countries, our infrastructure is designed to mitigate risk and ensure that your sourcing strategy is as robust as the chemistry we produce.
Precision in intermediate synthesis is non-negotiable. The transition from laboratory synthesis to full-scale commercial manufacturing requires a facility that operates with rigid adherence to process control and environmental standards. At our facility, we have replaced traditional manual variables with intelligent production automation, ensuring that every batch meets the stringent purity requirements demanded by downstream API manufacturers.
Our technical framework is built upon a foundation of international compliance, holding certifications from ISO9001 to NSF. This ensures that when you audit our drug substance intermediate factory capabilities, you are validating a system designed for traceability, safety, and efficiency. Below is an analysis of how our engineering standards translate into tangible technical advantages for your procurement needs.
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Process Consistency | Prevents batch-to-batch variation affecting drug efficacy. | Full Intelligent Production & Automatic Packaging | Eliminates human error, ensuring uniform purity profiles for Hydantoin derivatives. |
| Regulatory Compliance | Essential for global market entry and audit survival. | ISO9001, ISO14001, OHSAS18001, REACH, NSF | Seamless documentation integration for clients in regulated markets (US, EU). |
| Logistical Integrity | Prevents contamination and ensures timeline adherence. | Digital Storage & Standardized Loading Protocols | Zero cross-contamination risk and real-time inventory visibility. |
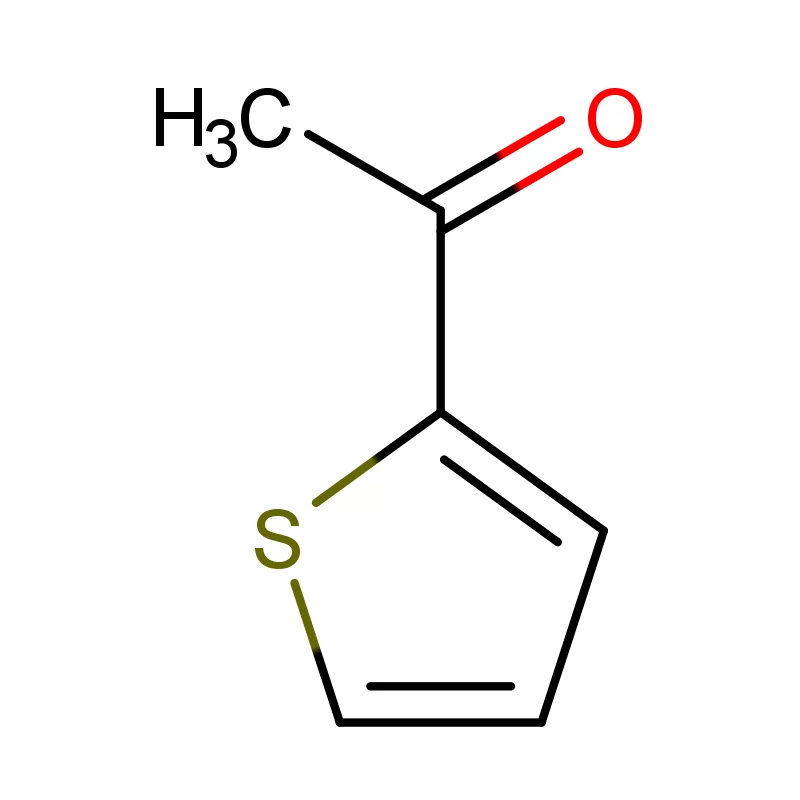
| Innovation Capacity | Ability to scale novel compounds. | Level 'A' R&D Institution Status | Rapid prototyping and scaling of complex Thiophene series intermediates. |
True Return on Investment (ROI) in chemical sourcing is not derived solely from unit price, but from the reduction of total cost of ownership (TCO). This includes minimizing the costs associated with re-validation, supply delays, and quality deviations. By partnering with a technologically advanced drug substance intermediate factory, pharmaceutical companies can transition from transactional purchasing to strategic value engineering. The stability provided by our automated facilities allows clients to reduce safety stock overheads and streamline their own quality control acceptance procedures.
Leache Chem's "Bromiguard" and "Dr. Brom" brands have sustained market dominance for over 20 years, proving that long-term reliability drives financial performance. Our win-win cooperation model focuses on optimizing the chemical pathway efficiency, directly impacting your bottom line. The chart below illustrates how our integrated manufacturing ecosystem improves supply consistency compared to conventional manufacturing benchmarks, securing your long-term profitability.
Related products
Top Selling Products