Email:
info@leachechem.com

The Challenge: In the complex landscape of chemical manufacturing, sourcing managers often face a critical dilemma: balancing high-purity requirements with supply chain consistency. Finding a partner that does not compromise on regulatory compliance or production capacity is essential for downstream success.
Leache Chem Ltd eliminates these uncertainties by operating as a tier-one solution provider. Established in 1991, our infrastructure is designed to solve the most pressing procurement challenges. Unlike generic suppliers, we function as a specialized fine chemicals solvents factory hub capable of supporting advanced industrial applications. Located in the Jingjin New Material Industrial Park, our facility leverages over three decades of operational expertise to deliver stability where others struggle.
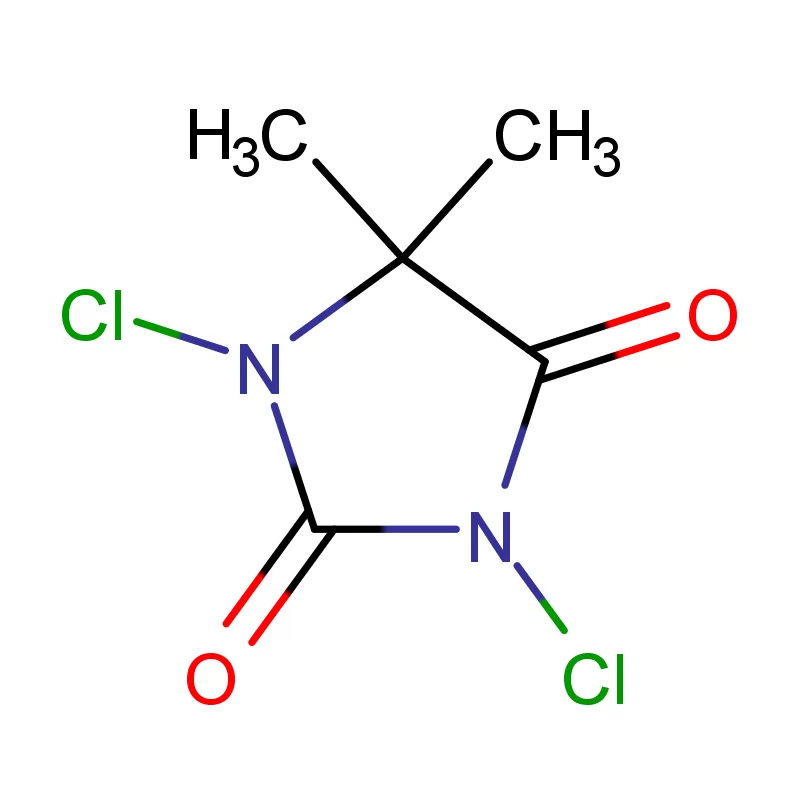
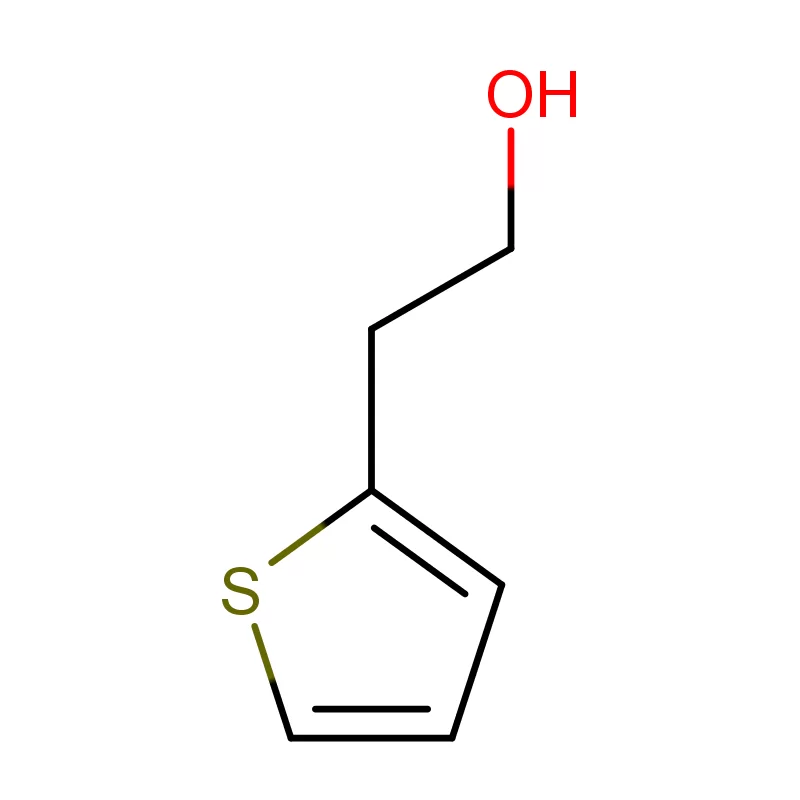
We understand that your production line cannot afford downtime or quality variance. By integrating intelligent production systems with a Hebei Province Level 'A' R&D Institution status, we ensure that every batch meets rigorous specifications. Whether you require hydantoin derivatives or thiophene series products, our approach transitions your supply chain from a transactional necessity to a strategic asset.
Operational excellence in chemical synthesis requires more than just raw capacity; it demands a convergence of intelligent engineering and strict protocol adherence. At Leache Chem, we define the benchmark for what a modern fine chemicals solvents factory should achieve. Our facility utilizes automatic packaging and digital storage systems to minimize human error and contamination risks, ensuring that the integrity of our 'Bromiguard' and 'Dr. Brom' product lines remains uncompromised.
Below represents our commitment to engineering precision compared to general industry expectations:
| Performance Metric | Industry Significance | Our Engineering Standard | Client Advantage |
|---|---|---|---|
| Quality Assurance System | Consistency across batches. | ISO9001 & Level 'A' R&D Institution validation. | Guaranteed purity levels reducing downstream filtration or refinement costs. |
| Regulatory Compliance | Market access and legality. | Comprehensive REACH, BSCI, & NSF Certifications. | Seamless export capabilities to strict markets like the EU and USA. |
| Production Logic | Efficiency and scalability. | Intelligent production with digital storage integration. | Faster turnaround times and real-time inventory visibility. |
| EHS (Environment, Health, Safety) | Sustainability and risk mitigation. | ISO14001 & OHSAS18001 Accredited. | Zero supply chain disruption due to environmental non-compliance. |
As the first high-tech enterprise in China to realize industrial production of 5,5-dimethylhydantoin, our technical pedigree is proven. This legacy of innovation ensures that when you engage with our factory, you are accessing a facility that leads rather than follows.
In today's volatile global market, the return on investment (ROI) from a chemical supplier is measured by longevity and scalability. Engaging with a proven fine chemicals solvents factory like Leache Chem offers distinct financial advantages. By centralizing production in our intelligent facility within the Economic Development Zone of Handan City, we pass on the efficiencies of scale and automation directly to our partners.
Our global footprint, extending to over 50 countries, attests to our ability to deliver value. Long-term cooperation with hundreds of clients proves that our independent brands, including 'Leache', deliver reliable performance that protects your bottom line. We move beyond simple manufacturing; we provide a "win-win" ecosystem where your growth is supported by our standardized loading and stable output.
Related products
Top Selling Products