Pharmaceutical Intermediates Solutions for Australia

Pharmaceutical Intermediates Solutions for Australia

Providing high-quality pharmaceutical intermediates, fine chemicals, and water treatment solutions to the Australian market.

Pharmaceutical Intermediates Solutions for Australia

Delivering reliable chemical solutions and expert support for the pharmaceutical and fine chemical industries in Australia.

Current Landscape of Chemical Manufacturing in Australia

An overview of the Australian chemical manufacturing market and its specific challenges and opportunities.

Australia’s chemical manufacturing sector is a vital component of its economy, yet it faces unique challenges due to its geographic isolation and relatively small domestic market. The demand for pharmaceutical intermediates is robust, driven by a growing healthcare sector and an aging population. The reliance on imports and the increasing costs of transportation are key considerations for businesses in this region.

The Australian climate, with its varying temperatures and water scarcity in certain areas, necessitates specialized industrial water treatment chemicals. Sustainable practices and environmentally responsible manufacturing are gaining increasing importance, pushing the industry towards greener technologies and processes.

The market for fine chemicals is particularly sensitive to regulatory changes and quality control requirements. Australia’s stringent regulations demand suppliers with proven track records and a commitment to compliance.

Evolution of Chemical Manufacturing in Australia

Tracing the development of the chemical industry in Australia from traditional methods to modern innovations.

Market Development History

Historically, Australia’s chemical industry was heavily reliant on basic commodity chemical production. From the mid-20th century, the industry began to diversify, driven by the needs of agriculture and mining. The 1980s saw an increased focus on specialty chemicals and 2 Bromothiophene, coinciding with the growth of the pharmaceutical sector.

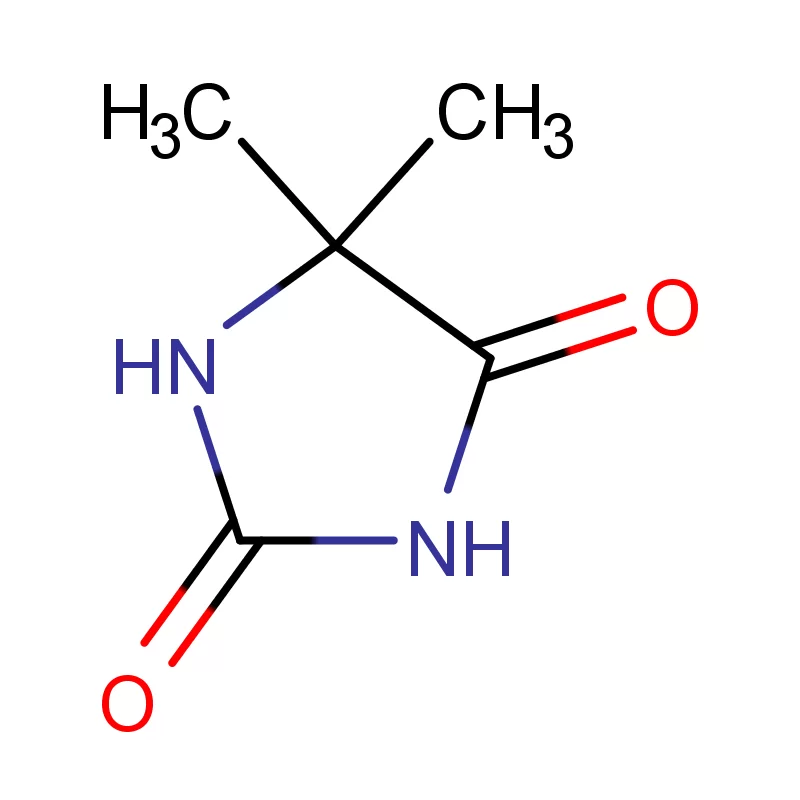
The late 1990s and early 2000s witnessed significant investment in research and development, leading to advancements in biotechnology and materials science. This period also saw the adoption of more sophisticated process control technologies and a greater emphasis on quality management systems. The demand for 5 5 Dimethyl Hydantoin has increased with growing cosmetic and industrial applications.

In recent years, the focus has shifted towards sustainable chemistry and the development of eco-friendly products. Government initiatives and consumer demand are driving the adoption of circular economy principles and the reduction of waste.

Future Development Trends

Advanced Materials Research

Australia is poised to become a leader in the development of advanced materials, particularly in areas such as polymers and composites. This will require significant investment in research infrastructure and collaboration between industry and academia.

Biotechnology and Biomanufacturing

The biotechnology sector is rapidly expanding, creating opportunities for the production of bio-based chemicals and pharmaceuticals. This trend is being fueled by the growing demand for sustainable alternatives to traditional petrochemicals.

Digitalization and Automation

The adoption of Industry 4.0 technologies, such as artificial intelligence, machine learning, and robotics, will transform the chemical manufacturing landscape. This will lead to increased efficiency, improved quality control, and reduced costs.
Industry Trends and Future Outlook for Australian Chemical Manufacturing

Exploring the key trends shaping the future of the chemical industry in Australia and the opportunities for growth.

Sustainable Chemistry Practices
Growing demand for eco-friendly chemical solutions and sustainable manufacturing processes in Australia.
Digital Transformation
Increased adoption of Industry 4.0 technologies for optimized production and supply chain management.
Supply Chain Resilience
Focus on diversifying supply chains and mitigating risks to ensure reliable access to critical chemicals.
Regulatory Compliance
Stringent adherence to Australian regulations and quality standards for chemical manufacturing.

Industry Outlook

The Australian chemical manufacturing sector is expected to experience moderate growth over the next five years, driven by the demand for specialized chemicals and sustainable solutions. The industry will continue to invest in research and development, automation, and supply chain resilience.

The rise of advanced materials and biotechnology will create new opportunities for innovation and growth. Collaboration between industry, academia, and government will be crucial for harnessing these opportunities and ensuring the long-term competitiveness of the Australian chemical industry.

Local Application Scenarios in Australia

Specific applications of our chemical products and solutions within the Australian context.

1. Pharmaceutical Manufacturing in Victoria

Supporting the production of essential medicines in Victoria’s thriving pharmaceutical industry with high-purity pharmaceutical intermediates and custom synthesis services.

2. Water Treatment for Mining Operations in Western Australia

Providing effective industrial water treatment chemicals to address water scarcity challenges in Western Australia’s mining sector.

3. Specialty Chemical Synthesis in New South Wales

Supplying fine chemicals for research and development applications in New South Wales’ biotechnology and pharmaceutical companies.

4. Polymer Production in Queensland

Offering 5 5 Dimethyl Hydantoin as a key ingredient in the production of high-performance polymers used in various industrial applications in Queensland.

Brand Story

The Global Development Journey of Hebei Lishe Chemical Technology Co., Ltd.

Foundation and Commitment to Quality

Established in [Year], Hebei Lishe Chemical Technology Co., Ltd. was founded on a commitment to providing high-quality chemical products and exceptional customer service.

Expansion into International Markets

Driven by a desire to serve a global clientele, we expanded our operations into international markets, including Australia, offering tailored solutions to meet specific regional needs.

Investment in R&D

We invested heavily in research and development to stay at the forefront of chemical innovation, developing new products and processes that address evolving industry challenges.

Sustainable Practices

We adopted sustainable manufacturing practices to minimize our environmental impact and promote responsible chemical management.

Customer-Centric Approach

We remain dedicated to building strong relationships with our customers, providing personalized support and reliable supply chain solutions.

Comprehensive Product Portfolio for the Australian Market

A diverse range of chemical products tailored to meet the needs of Australian industries.

Frequently Asked Questions – Australian Market

Addressing common questions about our products and services in Australia.

What are the lead times for delivering pharmaceutical intermediates to Australia?

Lead times vary depending on the specific product and quantity ordered. Typically, delivery to major Australian cities takes 7-14 business days.

Do your products meet Australian regulatory requirements for pharmaceutical manufacturing?

Yes, all our products are manufactured to meet the highest quality standards and comply with relevant Australian regulations, including those set by the TGA.

Can you provide custom synthesis services for specific chemical compounds?

Yes, we offer custom synthesis services tailored to meet your specific requirements. Our experienced team can develop and manufacture complex chemical compounds to your exact specifications.

What types of packaging do you offer for industrial water treatment chemicals in Australia?

We offer a variety of packaging options, including drums, IBCs, and bulk containers, to suit your specific needs and transportation requirements.

Do you offer technical support for the application of your fine chemicals?

Yes, our team of experienced chemists and engineers provides comprehensive technical support to assist you with the application of our fine chemicals.

What is your policy on sustainability and environmental responsibility?

We are committed to sustainable manufacturing practices and environmental responsibility. We strive to minimize our environmental impact and promote the safe and responsible handling of chemicals.

Get in Touch with Us

We’re here to help you find the right chemical solutions for your business in Oceania - Australia.

Contact Us Now

If you are interested in our products, you can choose to leave your information here, and we will be in touch with you shortly.