Pharmaceutical Intermediates Solutions for New Zealand

Pharmaceutical Intermediates Solutions for New Zealand

Delivering high-quality pharmaceutical intermediates, fine chemicals, and water treatment solutions to the New Zealand market.

Pharmaceutical Intermediates Solutions for New Zealand

Providing a comprehensive range of pharmaceutical intermediates, fine chemicals, and specialized chemical products tailored for the New Zealand pharmaceutical industry.

Current Landscape of Pharmaceutical Manufacturing in New Zealand

An overview of the pharmaceutical industry’s current state and challenges in New Zealand.

New Zealand's pharmaceutical industry is characterized by a strong emphasis on regulatory compliance and a growing demand for high-quality pharmaceutical intermediates. The relatively small domestic market necessitates a focus on niche product development and export opportunities, particularly within the Asia-Pacific region. Geographic isolation presents logistical challenges, driving demand for efficient supply chains and reliable sourcing of fine chemicals.

The industry is also influenced by New Zealand’s commitment to environmental sustainability, increasing the demand for environmentally friendly manufacturing processes and sustainable chemical sourcing. Water quality is a significant concern, leading to robust regulations regarding industrial water treatment chemicals. Competition from larger international markets requires New Zealand manufacturers to innovate and focus on specialized product offerings.

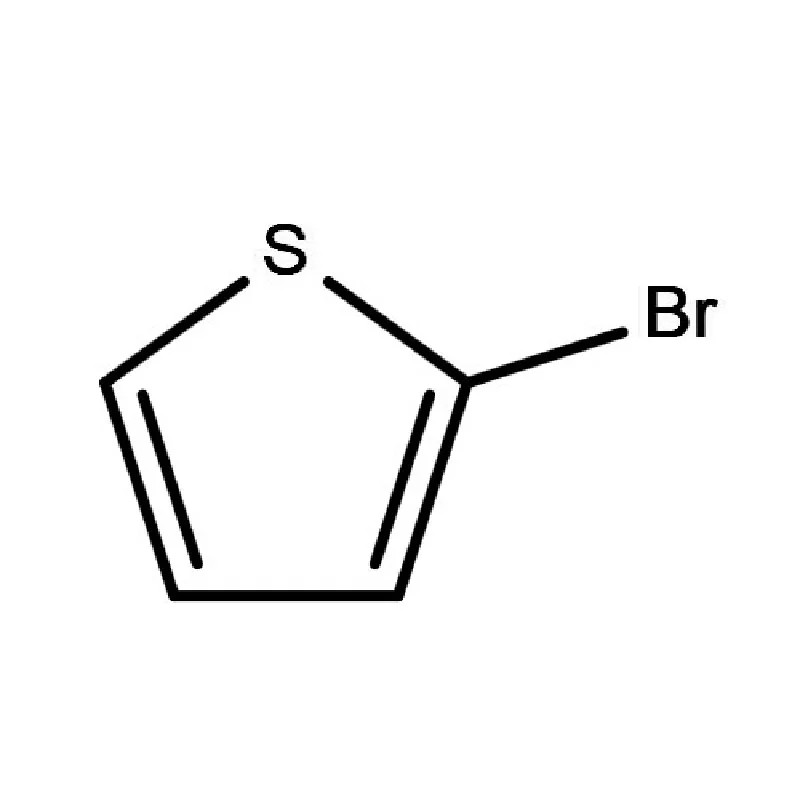
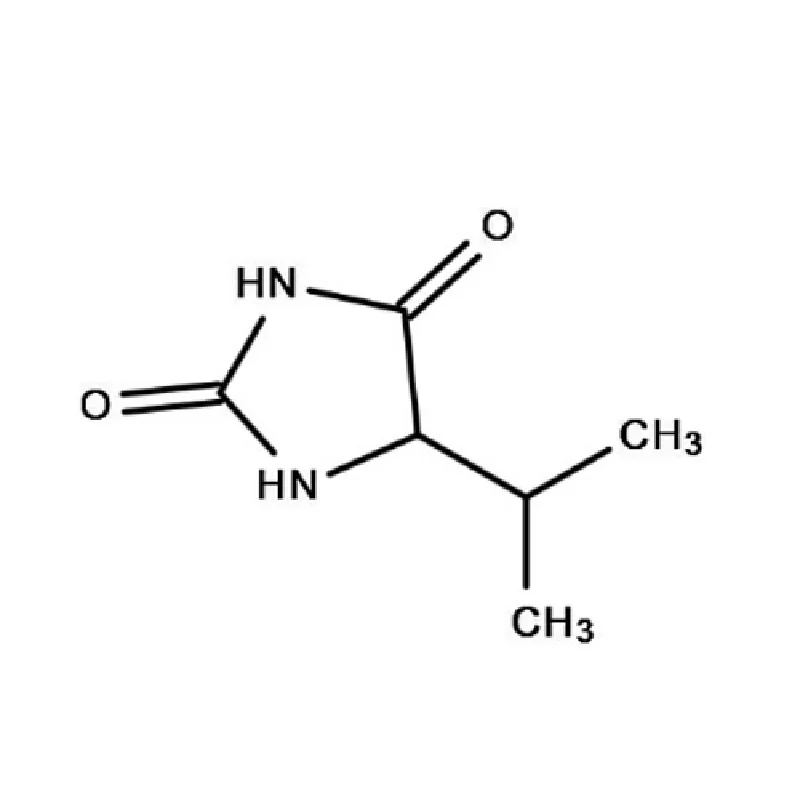
Furthermore, the aging population and increasing prevalence of chronic diseases are driving demand for innovative pharmaceuticals, boosting the need for specialized 2 Bromothiophene and other essential chemical building blocks. This heightened demand also pushes for reliable supply of 5 5 Dimethyl Hydantoin.

Evolution of Pharmaceutical Chemical Manufacturing in New Zealand

Tracing the development of the pharmaceutical chemical industry in New Zealand.

Market Development History

Initially, New Zealand's pharmaceutical chemical manufacturing focused largely on basic formulation and repackaging of imported active pharmaceutical ingredients (APIs). In the 1980s, increased investment in research and development led to the emergence of local companies specializing in the synthesis of pharmaceutical intermediates.

The 1990s saw the implementation of stricter regulatory standards, driving the need for improved quality control and analytical capabilities. This period also witnessed a growing emphasis on contract manufacturing for international pharmaceutical companies. The early 2000s brought advancements in green chemistry and sustainable manufacturing practices, influencing the selection of raw materials, including fine chemicals.

More recently, the industry has embraced advanced technologies such as continuous flow chemistry and biocatalysis to enhance efficiency and reduce environmental impact. The focus on industrial water treatment chemicals has increased due to environmental regulations.

Future Development Trends

Precision Chemistry and Custom Synthesis

The demand for highly specific chemical compounds is driving a trend towards precision chemistry and custom synthesis. This requires investment in advanced analytical equipment and highly skilled chemists.

Biocatalysis and Green Chemistry

Biocatalysis, using enzymes as catalysts, is gaining traction as a sustainable alternative to traditional chemical synthesis methods, reducing waste and energy consumption. 5 5 Dimethyl Hydantoin production can benefit from these greener approaches.

Digitalization and Automation

Implementing digital technologies such as AI and machine learning to optimize manufacturing processes, improve quality control, and enhance supply chain management will be crucial for maintaining competitiveness.

Industry Trends and Future Outlook for New Zealand

Analyzing emerging trends and forecasting the future of pharmaceutical chemical manufacturing in New Zealand.

Growing Demand for Specialty Chemicals
New Zealand's pharmaceutical sector is projected to experience a surge in demand for specialized chemicals, driven by innovative drug development and personalized medicine.
Increased Focus on Sustainability
Environmental regulations and consumer demand are driving a transition towards sustainable chemical manufacturing processes and the use of eco-friendly materials.
Supply Chain Resilience
Geopolitical instability and global disruptions are emphasizing the importance of building resilient and diversified supply chains.
Regulatory Harmonization
Increased efforts to harmonize pharmaceutical regulations across international markets will streamline product registration and market access.

Industry Outlook

The New Zealand pharmaceutical chemical industry is poised for moderate growth in the coming years, driven by a combination of domestic demand and export opportunities. Focus on sustainable manufacturing, investment in advanced technologies, and strong regulatory compliance will be critical for success.

Specifically, the demand for high-purity 2 Bromothiophene and specialized pharmaceutical intermediates will continue to rise, creating opportunities for innovative chemical manufacturers.

Local Application Scenarios in New Zealand

Examples of how our chemical products are used in New Zealand's pharmaceutical and related industries.

1. API Manufacturing for Local Generics

Supplying high-quality pharmaceutical intermediates to New Zealand-based generic drug manufacturers, reducing reliance on international sourcing and ensuring supply chain security.

2. Water Treatment in Pharmaceutical Production Facilities

Providing advanced industrial water treatment chemicals to maintain water purity and meet stringent regulatory standards in pharmaceutical manufacturing plants throughout New Zealand.

3. Research and Development of Novel Pharmaceuticals

Offering specialized fine chemicals and custom synthesis services to support research and development efforts at New Zealand universities and pharmaceutical companies.

4. Production of Veterinary Medicines

Supplying key chemical building blocks, including 5 5 Dimethyl Hydantoin, for the manufacture of veterinary pharmaceuticals used in New Zealand’s agricultural sector.

5. Biopharmaceutical Manufacturing Support

Providing high-purity chemicals and process solutions for the growing biopharmaceutical industry in New Zealand, ensuring product quality and regulatory compliance.

Brand Story

The Global Development Journey of Hebei Lishe Chemical Technology Co., Ltd.

Establishing a Foundation of Quality

Founded in 2008, Hebei Lishe Chemical Technology Co., Ltd. began with a commitment to delivering consistently high-quality chemical products. We initially focused on mastering core synthesis techniques for key pharmaceutical intermediates.

Expanding Product Portfolio

In 2012, we strategically expanded our product portfolio to include a wider range of fine chemicals and specialized compounds, catering to diverse pharmaceutical applications.

Investing in Sustainability

Recognizing the importance of environmental responsibility, we invested heavily in green chemistry technologies in 2016, minimizing waste and reducing our environmental footprint.

Global Reach and Partnerships

In 2018, we expanded our global reach through strategic partnerships, serving customers in key pharmaceutical markets worldwide, including New Zealand.

Commitment to Customer Success

Today, we remain dedicated to providing innovative chemical solutions, exceptional customer service, and unwavering quality, empowering our clients to succeed in the pharmaceutical industry.

Frequently Asked Questions - New Zealand

Addressing common questions from our customers in New Zealand.

What is the typical lead time for delivery of pharmaceutical intermediates to New Zealand?

Lead times vary depending on the specific product and quantity ordered. Generally, you can expect delivery within 10-14 business days, including customs clearance.

Do you provide Certificates of Analysis (COAs) for your fine chemicals?

Yes, we provide comprehensive Certificates of Analysis (COAs) for all our fine chemicals, detailing product specifications and analytical results.

What regulatory compliance standards do you adhere to for pharmaceutical intermediates?

We adhere to strict quality control standards, including ISO 9001 certification, and ensure our products meet relevant pharmaceutical regulations.

Can you provide custom synthesis services for specialized chemical compounds?

Yes, we offer custom synthesis services to meet specific research and development needs, including the synthesis of 2 Bromothiophene.

What types of packaging options are available for industrial water treatment chemicals?

We offer a range of packaging options, including drums, IBCs, and bulk containers, to suit your specific requirements.

Do you offer technical support for the application of your products?

Yes, our team of experienced chemists and engineers provides comprehensive technical support to assist you with product application and optimization.

Get in Touch with Us

We are dedicated to providing chemical solutions to the pharmaceutical industry in New Zealand. Contact us today to discuss your specific requirements.

Contact Us Now

If you are interested in our products, you can choose to leave your information here, and we will be in touch with you shortly.