Email:
info@leachechem.com


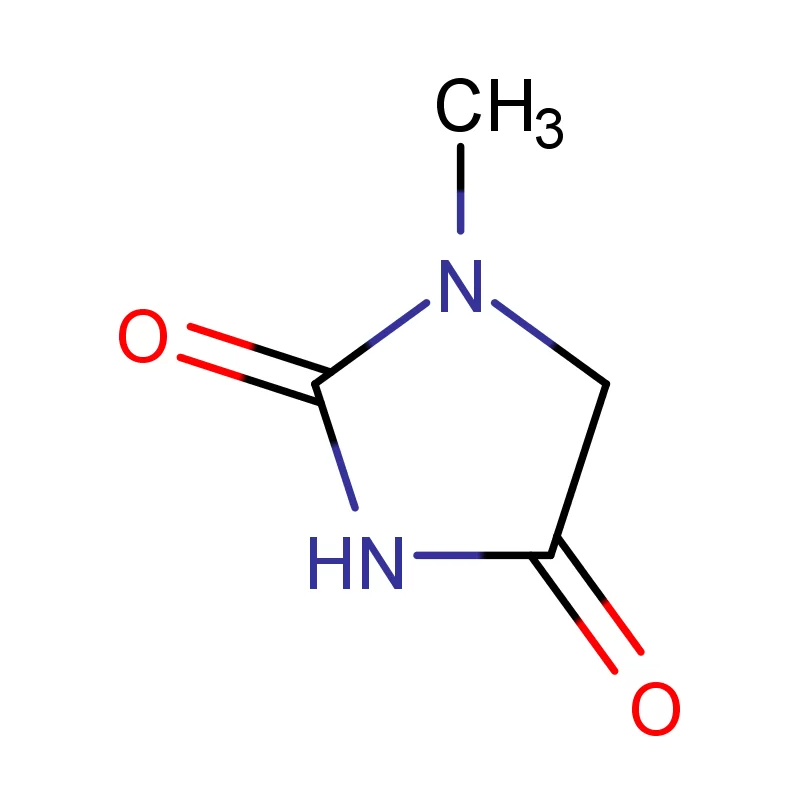
1-Methylhydantoin is a high-purity, white crystalline compound engineered as a versatile pharmaceutical intermediate for advanced chemical synthesis. With a guaranteed purity exceeding 98.5%, this critical building block is indispensable for the development of high-precision pharmaceutical formulations, specialty polymers, and sophisticated agrochemical products.
Its stable chemical structure ensures seamless compatibility across diverse industrial processes, providing a reliable foundation for synthesizing bioactive molecules. From oncology and neurology drug development to high-performance dielectric precursors in electronics, 1-Methylhydantoin enables efficient synthesis routes and superior end-product stability.
| Appearance | White to off-white powder | Purity (%) | ≥98.5% |
|---|---|---|---|
| Melting Point (°C) | 165–172°C | pH (5% solution) | 5.0–7.0 |
| Moisture Content | ≤0.5% | Chemical Nature | Pharmaceutical Intermediate |
| Stability | High thermal stability | Solubility | Compatible with organic solvents |
| Application Grade | Industrial/Pharmaceutical | Storage Condition | Cool, dry environment |
Maintaining a purity level of ≥98.5%, ensuring consistent reaction yields and minimal impurity profiles in pharmaceutical synthesis.
Robust chemical architecture provides exceptional stability during complex crosslinking and synthesis processes.
Effective in pharmaceutical, agrochemical, electronic, and polymer coating sectors for maximum versatility.
Ideal for synthesizing anticonvulsants, nootropic agents, and high-value molecules in neurology and oncology.
Optimized for use in epoxy resin crosslinking and stabilizing halogenated compounds in water treatment.
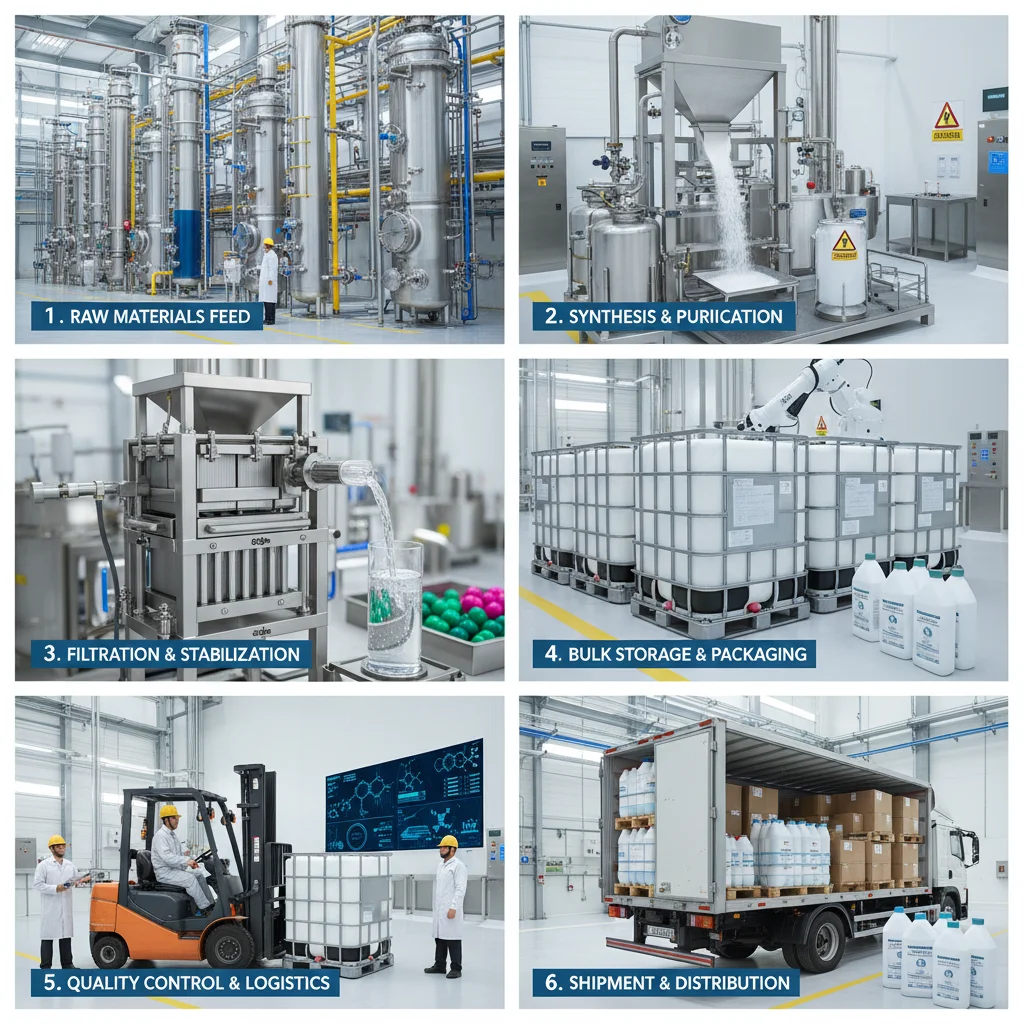
Manufactured and packaged according to international safety and quality standards for global distribution.
Dual-layer protection with food-grade PE liners and UV-resistant woven PP bags.
Stringent testing protocols ensuring each batch meets exact purity and moisture specifications.
Flexible sizing from 20kg cartons to 500kg bulk containers to fit your production scale.
Continuous technical optimization to provide high-efficiency synthesis routes for clients.
Integrated supply chain management ensuring timely delivery and material integrity worldwide.
30+ years of manufacturing expertise providing tailored technical solutions for complex synthesis.
| Feature | Standard Grade | Leache Premium Grade |
|---|---|---|
| Purity Level | <98% | ≥98.5% |
| Synthesis Yield | Moderate | High-Efficiency |
| Impurity Profile | Variable | Strictly Controlled |
| Stability Period | Standard | Extended Shelf-life |
| Technical Support | Basic | Expert Consultation |
It is primarily used as a critical intermediate for synthesizing anticonvulsants, nootropic agents, and bioactive molecules, specifically within oncology and neurology drug development.
Beyond medicine, it serves as a crosslinking agent in epoxy resins, a stabilizer for halogenated compounds in water treatment, and a dielectric precursor in electronics.
We offer standard 20kg cartons and 500kg bulk containers, utilizing food-grade PE liners and UV-resistant woven PP bags to ensure product integrity during transit.
A purity of ≥98.5% minimizes side reactions and impurity buildup, leading to higher conversion rates and more efficient purification processes in high-precision applications.
Yes, all our packaging and handling procedures comply with international safety standards to guarantee secure storage and safe transit across global borders.
Leache brings 30+ years of manufacturing expertise, combining stringent quality control, an R&D-driven approach, and a global supply chain to provide unmatched technical support.