High Purity 5 5 Dimethylhydantoin factory for Water Treatment

0%

Table of Contents

The industrial landscape of water treatment has evolved rapidly, placing a premium on high-efficiency biocides that can withstand rigorous operational conditions. Central to this evolution is the role of a specialized 5 5 Dimethylhydantoin factory, which focuses on producing high-purity intermediates and active agents like DBDMH to ensure systemic hygiene. Understanding the synergy between precise chemical manufacturing and industrial application is essential for maintaining the longevity of cooling infrastructure globally.

From a global perspective, the demand for robust disinfection solutions is driven by the need to prevent biofouling in power plants and petrochemical facilities. A professional 5 5 Dimethylhydantoin factory provides the critical raw materials needed to produce bromine-based chemicals that offer superior oxidative efficiency. These solutions are not merely additives but are fundamental to reducing operational downtime and preventing costly corrosion in large-scale recirculating systems.

By integrating advanced synthesis techniques, the output from a leading 5 5 Dimethylhydantoin factory ensures that products like DBDMH maintain a purity exceeding 98%. This level of quality control allows industrial operators to implement automated dosing systems with confidence, knowing that the active bromine release will be steady and predictable. The following analysis explores the technical dimensions, applications, and future trends associated with these essential chemical precursors.

5 5 Dimethylhydantoin factory

The Role of a 5 5 Dimethylhydantoin factory in Chemical Synthesis

5 5 Dimethylhydantoin factory

A dedicated 5 5 Dimethylhydantoin factory serves as the foundational link in the production of bromine-based disinfectants. By synthesizing the hydantoin ring structure with precision, these facilities enable the creation of DBDMH, a potent agent designed for the gradual release of active bromine. This controlled release is critical for maintaining a consistent residual concentration of disinfectant in complex water loops, preventing the sudden spikes or drops that can lead to microbial breakthroughs.

The engineering expertise within a 5 5 Dimethylhydantoin factory focuses on optimizing the reaction kinetics to ensure that the resulting white crystalline powder is free from impurities. This ensures that when the product is applied in industrial settings, it does not introduce unwanted contaminants into the process water, thereby protecting sensitive heat exchangers and preventing unexpected chemical reactions in high-pressure environments.

Technical Specifications and Purity Standards

The efficacy of any industrial water treatment chemical is dictated by its purity. Products originating from a high-standard 5 5 Dimethylhydantoin factory typically boast an active ingredient concentration of ≥98%. This high purity level is non-negotiable for large-scale operations where even a 1% variance in quality can lead to significant dosing inaccuracies and increased waste.

Physically, the product is characterized as a white crystalline powder with a pH range of 6.0 to 9.0. This neutrality is essential for its compatibility with diverse water chemistries, ensuring that it does not drastically shift the pH of the treated system, which could otherwise trigger scaling or accelerate metallic corrosion in piping and cooling towers.

Furthermore, the gradual release solubility is a key technical advantage. Unlike rapid-dissolve chemicals that provide a short-lived "shock" treatment, the synthesis managed by a professional 5 5 Dimethylhydantoin factory ensures a sustained oxidative effect. This reduces the frequency of manual interventions and lowers the total volume of chemical required over a fiscal quarter.

Mechanisms of Biofouling Control and Disinfection

Biofouling presents a severe threat to industrial efficiency, as biofilm layers act as insulators, drastically reducing heat transfer in exchangers. The output from a 5 5 Dimethylhydantoin factory provides the bromine source necessary to penetrate these extracellular polymeric substances (EPS) and eliminate the underlying bacteria.

The bromine released via DBDMH is more effective than chlorine in alkaline conditions, which are common in industrial cooling loops. By utilizing the high-purity precursors from a 5 5 Dimethylhydantoin factory, facilities can maintain an oxidative environment that aggressively combats algae and slime-forming bacteria without the volatility associated with liquid bleach.

Ultimately, the ability to control microbial growth even under high organic loads is what distinguishes the grade of chemicals produced at a professional 5 5 Dimethylhydantoin factory. This ensure that the disinfection process is robust enough to handle industrial wastewater and process water that may contain various organic contaminants.

Operational Efficiency in Industrial Cooling Systems

Implementing a dosing strategy based on materials from a 5 5 Dimethylhydantoin factory leads to a measurable reduction in maintenance costs. Because the active bromine is released steadily, the "sawtooth" effect of chemical concentrations is smoothed out, leading to a more stable environment for the equipment.

The integration of these chemicals into automated dosing systems allows for real-time adjustments based on water quality sensors. This synergy between chemical stability and digital control maximizes the ROI for plant managers, ensuring that the system is never under-treated (risking biofouling) or over-treated (wasting expensive chemicals).

Comparative Efficiency of 5 5 Dimethylhydantoin factory Grade Chemicals

Global Application across Heavy Industries

The versatility of chemicals produced by a 5 5 Dimethylhydantoin factory makes them indispensable in power generation. In these facilities, cooling loops must operate at peak efficiency to maintain turbine temperatures; any biofilm buildup can lead to catastrophic overheating or forced outages.

Beyond power plants, the petrochemical sector relies on these bromine-based agents for process water treatment. Given the high organic loads and harsh environments typically found in refineries, the stability provided by a high-purity 5 5 Dimethylhydantoin factory ensures that the disinfection process remains effective without compromising the integrity of the infrastructure.

Safety, Logistics, and International Standards

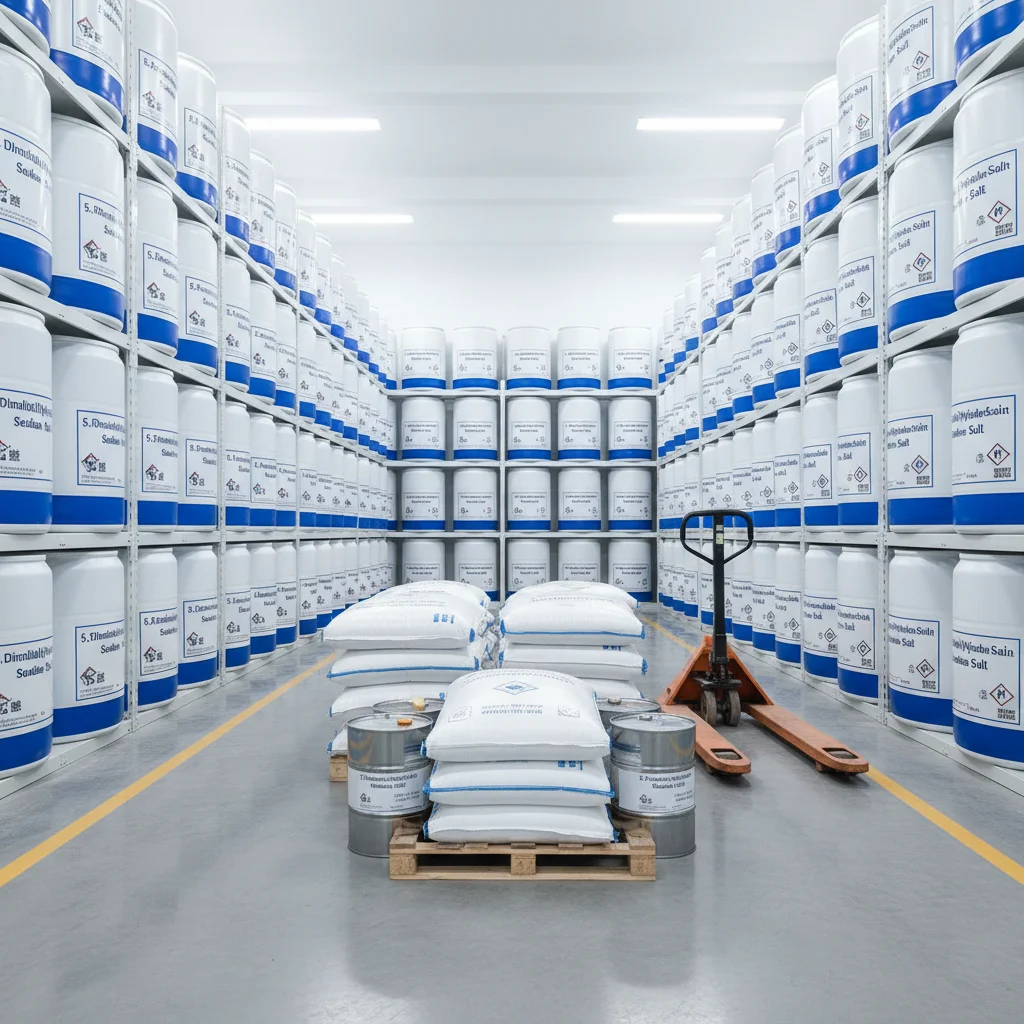
Handling hazardous industrial chemicals requires strict adherence to global safety protocols. A reputable 5 5 Dimethylhydantoin factory ensures that all packaging—typically 25 kg polyethylene-lined fiber drums—meets international safety standards for the transport of hazardous materials. This prevents leakage and contamination during global transit.

Logistical efficiency is further enhanced through customized bulk quantity options, allowing large-scale manufacturing units to reduce their carbon footprint by minimizing the number of shipments. The rigorous quality documentation provided by the 5 5 Dimethylhydantoin factory facilitates seamless customs clearance and regulatory compliance across different jurisdictions.

Moreover, the commitment to non-corrosive disinfection means that operators can handle these products with a higher degree of safety compared to concentrated liquid acids or bases. This focus on safety and stability is a hallmark of a modern, professional 5 5 Dimethylhydantoin factory.

Future Innovations in Hydantoin-Based Chemistry

The future of water treatment is leaning toward "green chemistry" and digital transformation. A forward-thinking 5 5 Dimethylhydantoin factory is now exploring ways to further reduce residual byproducts while maintaining high oxidative efficiency. This involves refining the synthesis process to eliminate trace impurities that can contribute to environmental load.

Automation is also playing a key role, with the development of "smart pellets" that can dissolve at varying rates based on the water temperature and flow rate. By collaborating with IoT sensor manufacturers, a 5 5 Dimethylhydantoin factory can help create a closed-loop system where the chemical supply is adjusted in real-time to match the microbial load.

As global water scarcity increases, the need for highly efficient recirculating systems will only grow. The ongoing innovations at the 5 5 Dimethylhydantoin factory will be pivotal in enabling industries to reuse water more aggressively without risking biological contamination.

Analysis of 5 5 Dimethylhydantoin factory Production and Application Metrics

Metric Category Standard Factory Output Premium Factory Grade Industrial Impact
Chemical Purity 95% - 97% ≥98% Higher Oxidative Efficiency
Dissolution Rate Irregular Gradual/Steady Reduced Dosing Frequency
pH Stability Fluctuating 6.0 - 9.0 Lower Corrosion Risk
Biofilm Penetration Moderate Excellent Improved Heat Transfer
Packaging Compliance Basic International Hazmat Secure Global Logistics
System Compatibility Limited Universal/Automated Lower Operational Cost

FAQS

What is the primary advantage of sourcing from a specialized 5 5 Dimethylhydantoin factory?

The primary advantage is the guarantee of high purity (≥98%) and precise chemical stability. A specialized factory ensures that the DBDMH produced has a consistent gradual-release profile, which is essential for preventing biofouling in industrial cooling systems without causing pH spikes or corrosive damage to equipment.

How does the product from a 5 5 Dimethylhydantoin factory compare to chlorine-based treatments?

Unlike chlorine, the bromine-based chemicals synthesized in a 5 5 Dimethylhydantoin factory remain highly effective in alkaline water conditions. They also provide a more stable residual concentration and are generally less corrosive to metal surfaces in heat exchangers and piping.

Is the packaging from a 5 5 Dimethylhydantoin factory safe for international shipping?

Yes, professional factories utilize polyethylene-lined fiber drums that meet international hazardous materials safety standards. This ensures that the white crystalline powder remains dry and secure, preventing any accidental release during sea or air freight.

Can DBDMH be integrated into automated dosing systems?

Absolutely. Because of its predictable solubility and high purity, DBDMH produced by a leading 5 5 Dimethylhydantoin factory is ideal for automated systems. It allows for consistent performance and reduced manual labor in large-scale petrochemical or power plant operations.

What pH range is typical for chemicals coming from a 5 5 Dimethylhydantoin factory?

The typical pH range is between 6.0 and 9.0. This neutral-to-slightly-alkaline range ensures that the chemical is compatible with most industrial water chemistries and does not necessitate extensive pH buffering after application.

How does a 5 5 Dimethylhydantoin factory handle bulk customized orders?

Most professional factories offer tailored packaging solutions and bulk quantities to meet the specific needs of large industrial units. This includes customized drum sizes or super-sacks to optimize logistics and reduce the cost per kilogram for the end-user.

Conclusion

In summary, the operational success of industrial water treatment relies heavily on the quality of the chemical precursors provided by a 5 5 Dimethylhydantoin factory. From maintaining a purity of ≥98% to ensuring a steady release of active bromine, these factors collectively prevent biofouling, protect infrastructure from corrosion, and reduce long-term operational costs. The synergy between high-grade chemical synthesis and automated industrial application represents the gold standard for modern disinfection.

Looking forward, the integration of greener synthesis methods and smart dosing technologies will further enhance the value provided by the 5 5 Dimethylhydantoin factory. For industries aiming to optimize their cooling efficiency and sustainability, partnering with a manufacturer that adheres to strict international safety and purity standards is not just an operational choice, but a strategic necessity. Visit our website: www.leache-chem.com
William Thompson

William Thompson

William Thompson is a Senior Production Engineer at Leache Chem, overseeing the automated packaging and digital storage systems implemented in the provincial industrial park. He joined the company in 2016, bringing extensive experience in process engineering and automation. William was crucial in transitioning the production lines to intelligent manufacturing, enhancing
Previous Professional 5 5 Dimethylhydantoin manufacturer for API Synthesis
Next High Purity 5 5 Dimethylhydantoin exporter for Fine Chemicals

If you are interested in our products, you can choose to leave your information here, and we will be in touch with you shortly.