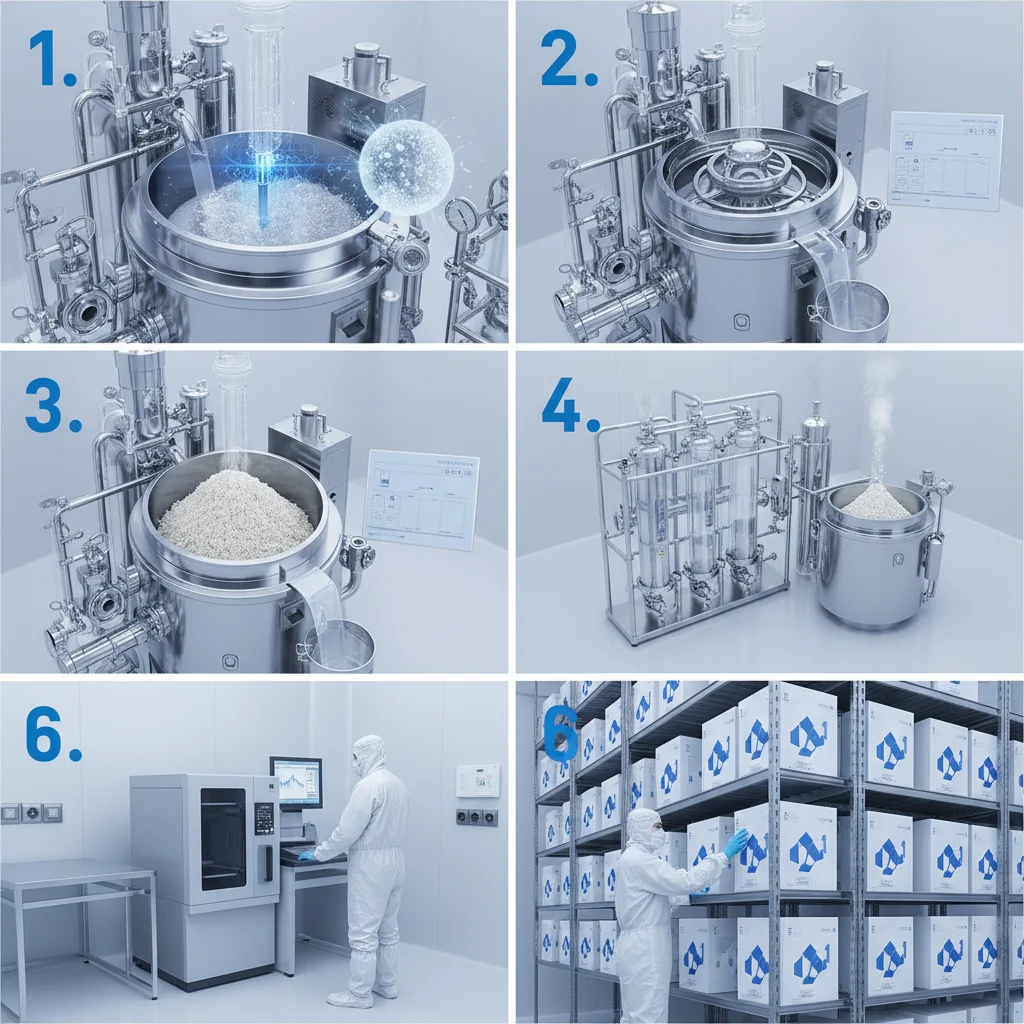
The global demand for high-efficiency disinfecting agents and pharmaceutical intermediates has led to a significant increase in the strategic importance of the 5 5 DimethylHydantoin Sodium Salt factory. As industries strive for higher purity and more stable chemical precursors, the role of specialized manufacturing facilities becomes paramount in ensuring the safety and efficacy of water treatment and chemical synthesis.
In the context of modern industrial hygiene and pharmaceutical synthesis, the ability to produce stabilized oxidants is critical. A dedicated 5 5 DimethylHydantoin Sodium Salt factory provides the necessary infrastructure to maintain rigorous quality standards, ensuring that the final products—such as dibromo hydantoin—meet the strict purity requirements of the global healthcare and environmental sectors.
Understanding the operational capabilities of a 5 5 DimethylHydantoin Sodium Salt factory allows procurement managers and chemists to optimize their supply chains for high-performance bromating agents and disinfectants. By leveraging precision manufacturing, these facilities deliver essential chemicals that protect public health through advanced sterilization and support the creation of complex organic molecules.

Global Industry Context of 5 5 DimethylHydantoin Sodium Salt factory
The chemical manufacturing landscape is currently undergoing a transition toward more specialized, high-purity intermediates. For a 5 5 DimethylHydantoin Sodium Salt factory, this means adhering to stringent international standards to serve the pharmaceutical and water treatment industries. With global health organizations emphasizing the need for sterile environments and clean water, the production of stabilized brominating agents has become a cornerstone of industrial hygiene.
Furthermore, the integration of these chemicals into the pharmaceutical supply chain highlights the necessity of reliable factory output. The ability to synthesize high-purity precursors consistently is what separates a standard chemical plant from a specialized 5 5 DimethylHydantoin Sodium Salt factory, ensuring that downstream drug synthesis is not compromised by impurities.
Definition and Technical Meaning
In simple technical terms, a 5 5 DimethylHydantoin Sodium Salt factory is a specialized facility focused on the production of hydantoin derivatives. These chemicals serve as the structural basis for powerful disinfectants and organic synthesis agents. The resulting products, such as dibromo hydantoin, typically appear as light yellow or off-white crystal powders with a high purity level (≥98%) and a significant bromo content (≥54.8%).
The importance of this facility lies in its ability to control the chemical stability of the output. Because these products are used as streamlined oxidant-type disinfecting agents, they must be stable when dry yet soluble in organic solvents like chloroform and ethanol. This specific chemical profile allows them to be used effectively in various forms, including granules and tablets.
Beyond simple disinfection, the outputs from a 5 5 DimethylHydantoin Sodium Salt factory are indispensable in the realm of organic chemistry. They act as excellent industrial bromating agents, facilitating the creation of complex pharmaceutical intermediates that would be difficult to synthesize using less stable bromine sources.
Key Quality Factors and Core Components
One of the primary quality markers for any 5 5 DimethylHydantoin Sodium Salt factory is the precision of the melting point, typically maintained between 185~192℃. This range ensures that the chemical remains stable during transport and storage, preventing premature decomposition that could reduce the efficacy of the brominating agent.
The purity level is another critical component; a top-tier 5 5 DimethylHydantoin Sodium Salt factory ensures purity is ≥98% with a drying loss of ≤0.5%. This level of refinement is essential for applications in pharmaceutical intermediates, where even trace impurities can trigger adverse reactions or fail quality control audits in drug manufacturing.
Finally, the environmental impact and biodegradation are core considerations. Products from a 5 5 DimethylHydantoin Sodium Salt factory are designed to be biodegradable in a short time without causing pollution, particularly when used within the optimal pH range of 5~7 for antisepsis.
Global Applications and Use Cases
The versatility of products from a 5 5 DimethylHydantoin Sodium Salt factory allows them to be deployed across diverse sectors. In the public health domain, they are used for the sterilization of swimming pools, tap water, and the environment of hotels and hospitals. The slow-release nature of these oxidants makes them ideal for maintaining long-term sanitary conditions in high-traffic public spaces.
In the industrial and agricultural sectors, these chemicals are vital for aquaculture sterilization and industrial water treatment. By preventing biofouling and microbial growth in cooling towers and fish farms, the output of a 5 5 DimethylHydantoin Sodium Salt factory helps maintain productivity and prevent massive losses due to waterborne pathogens.
Performance Metrics of 5 5 DimethylHydantoin Sodium Salt factory Outputs
Advantages and Long-Term Value
The long-term value of partnering with a certified 5 5 DimethylHydantoin Sodium Salt factory lies in the reliability of the chemical properties. Because the products are bland with a light odor and offer slow-release capabilities, they reduce the frequency of application and the risk of chemical burns or irritation compared to harsher, fast-acting oxidants.
From a sustainability perspective, the biodegradability of these compounds ensures that industrial water treatment does not lead to long-term ecological damage. This aligns with global ESG (Environmental, Social, and Governance) goals, making the output of a 5 5 DimethylHydantoin Sodium Salt factory a preferred choice for companies aiming for green certifications.
Future Trends and Innovations
Looking forward, the 5 5 DimethylHydantoin Sodium Salt factory is expected to integrate more automation and digital monitoring into the production process. By utilizing real-time sensors to monitor the purity and bromo content during synthesis, factories can achieve even tighter tolerances, potentially pushing purity levels beyond 99%.
There is also a growing trend toward the development of customized physical forms. While crystal powder is the standard, the transition toward precisely engineered tablets and granules allows for more controlled dosing in swimming pools and industrial systems, reducing chemical waste.
Furthermore, the synergy between these factories and the pharmaceutical industry is deepening. As new drug molecules are discovered, the demand for specialized bromating agents will evolve, prompting the 5 5 DimethylHydantoin Sodium Salt factory to innovate new derivative salts that offer even higher reactivity or specific solubility profiles.
Challenges and Expert Solutions
One of the primary challenges faced by a 5 5 DimethylHydantoin Sodium Salt factory is the sensitivity of the product to environmental conditions. Since the chemical is easy to decompose in strong acids and strong alkalis, maintaining a strict pH environment during processing and storage is critical to prevent degradation.
Another limitation is the requirement for specialized transportation. To prevent solarization and drenching, the product must be packed in double-layer non-poisonous plastic sealed bags and transported as common chemicals but strictly separated from poisonous substances. This logistical complexity requires a high level of operational expertise.
To overcome these challenges, expert factories implement climate-controlled storage facilities and use high-grade cardboard barrels or woven bags for external protection. By ensuring a cool, dry environment and strict adherence to handling protocols, the two-year validity period of the product is guaranteed.
Technical Analysis of 5 5 DimethylHydantoin Sodium Salt factory Quality Standards
|
Quality Metric
|
Standard Specification
|
Industrial Importance
|
Compliance Score (1-10)
|
| Purity Level |
≥98% |
Critical for Pharma Intermediates |
10 |
| Bromo Content |
≥54.8% |
Determines Oxidizing Power |
9 |
| Melting Point |
185~192℃ |
Indicates Thermal Stability |
9 |
| Drying Loss |
≤0.5% |
Prevents Caking and Clumping |
8 |
| pH Efficacy |
5~7 Range |
Optimal Antisepsis Activity |
10 |
| Biodegradability |
Short-term |
Environmental Safety |
8 |
FAQS
A high-quality product typically features a purity of ≥98%, a bromo content of ≥54.8%, and a melting point between 185~192℃. Additionally, the drying loss should be ≤0.5% to ensure the stability of the crystal powder and its effectiveness as an industrial bromating agent.
Yes, products from a 5 5 DimethylHydantoin Sodium Salt factory are widely used as streamlined oxidant-type disinfecting agents for swimming pools and tap water. They are valued for being bland, having a light odor, and providing a slow-release mechanism for consistent sterilization.
The product should be kept in a cool and dry place, avoiding contact with injurant materials to prevent pollution. It is critical to keep it away from strong acids and strong alkalis, as it decomposes easily under those conditions. Properly stored, it has a validity of two years.
Yes, the dibromo hydantoin produced is designed to be biodegradable in a short time without causing pollution. This makes it an excellent choice for aquaculture and industrial water treatment where ecological impact is a primary concern.
Standard packaging includes a non-poisonous plastic sealed inner bag with an outer layer of woven bags, plastic barrels, or cardboard barrels. The typical net weight is 25Kg per unit, although customization is available based on customer requirements.
Absolutely. Beyond disinfection, it serves as an excellent industrial bromating agent. It is frequently used by pharmaceutical companies to synthesize various organic chemicals and complex pharmaceutical intermediates due to its high stabilization and purity.
Conclusion
In summary, the operations of a 5 5 DimethylHydantoin Sodium Salt factory are central to the production of high-purity disinfectants and pharmaceutical intermediates. By maintaining strict standards for purity, bromo content, and thermal stability, these facilities provide the critical chemical building blocks required for everything from public health sterilization to advanced drug synthesis. The combination of high efficacy and environmental biodegradability ensures that these products remain viable in an increasingly regulated global market.
As the industry moves toward greener chemistry and greater automation, the role of the specialized factory will only grow in significance. For companies seeking reliable, high-performance bromating agents or water treatment chemicals, prioritizing a supplier with a proven track record in quality control and stable logistics is essential. We invite you to explore our capabilities and ensure your supply chain is powered by the best in chemical engineering. Visit our website: www.leache-chem.com