The global demand for high-purity pharmaceutical intermediates has led to an increased focus on the operational excellence of a specialized DMH factory. As the chemical industry pivots toward more stringent quality standards, the production of 1,3-Dimethylol-5,5-Dimethyl Hydantoin (DMH) has become a cornerstone for synthesizing advanced APIs and specialty drugs. Understanding the capabilities of a modern production facility is essential for procurement managers and researchers seeking consistency in their chemical supply chains.
Within the pharmaceutical and fine chemical sectors, the stability and purity of raw materials directly impact the efficacy of the final therapeutic agent. A professional DMH factory employs rigorous synthesis protocols to ensure that the molecular structure remains stable, which is critical for high-value formulations. This commitment to precision prevents impurities from compromising the integrity of life-saving drugs, thereby reducing the risk of batch failure during pilot-scale production.
Choosing a reliable DMH factory ensures that industries receive materials with a purity exceeding 99%, meeting international safety and quality protocols. By integrating advanced moisture control and solubility optimization, these facilities support a wide range of applications from water treatment biocides to sophisticated electronic components.

The Role of a DMH Factory in API Synthesis
A specialized DMH factory serves as the primary engine for producing 1,3-Dimethylol-5,5-Dimethyl Hydantoin, a multifunctional compound essential for the creation of active pharmaceutical ingredients (APIs). By focusing on the synthesis of high-purity intermediates, these factories enable pharmaceutical companies to accelerate the development of complex therapeutic agents, ensuring that each molecular building block meets precise geometric and chemical requirements.
The synergy between chemical engineering and pharmaceutical science within such a facility allows for the optimization of reaction yields. This ensures that the DMH produced is not only chemically pure but also physically consistent, which is a prerequisite for the stringent quality requirements of the global medical market.
Technical Specifications and Purity Standards
The technical benchmarks set by a leading DMH factory are designed to eliminate contaminants that could interfere with subsequent chemical reactions. With a purity level maintained at ≥99%, the product ensures that researchers in R&D laboratories can achieve reproducible results during pilot-scale production, reducing the need for costly recrystallization steps.
Moisture content is another critical parameter, strictly controlled to ≤0.5%. Excessive moisture can lead to degradation or unwanted side reactions during the synthesis of specialty drugs, making the anhydrous nature of the crystalline powder a key value proposition for high-end chemical manufacturing.
Furthermore, the solubility profile—being compatible with both water and organic solvents—makes this compound exceptionally adaptable. This dual-compatibility allows a DMH factory to supply materials that are easily integrated into various solvent systems, facilitating a smoother workflow in both liquid-phase and solid-phase synthesis.
Versatile Industrial Applications of DMH
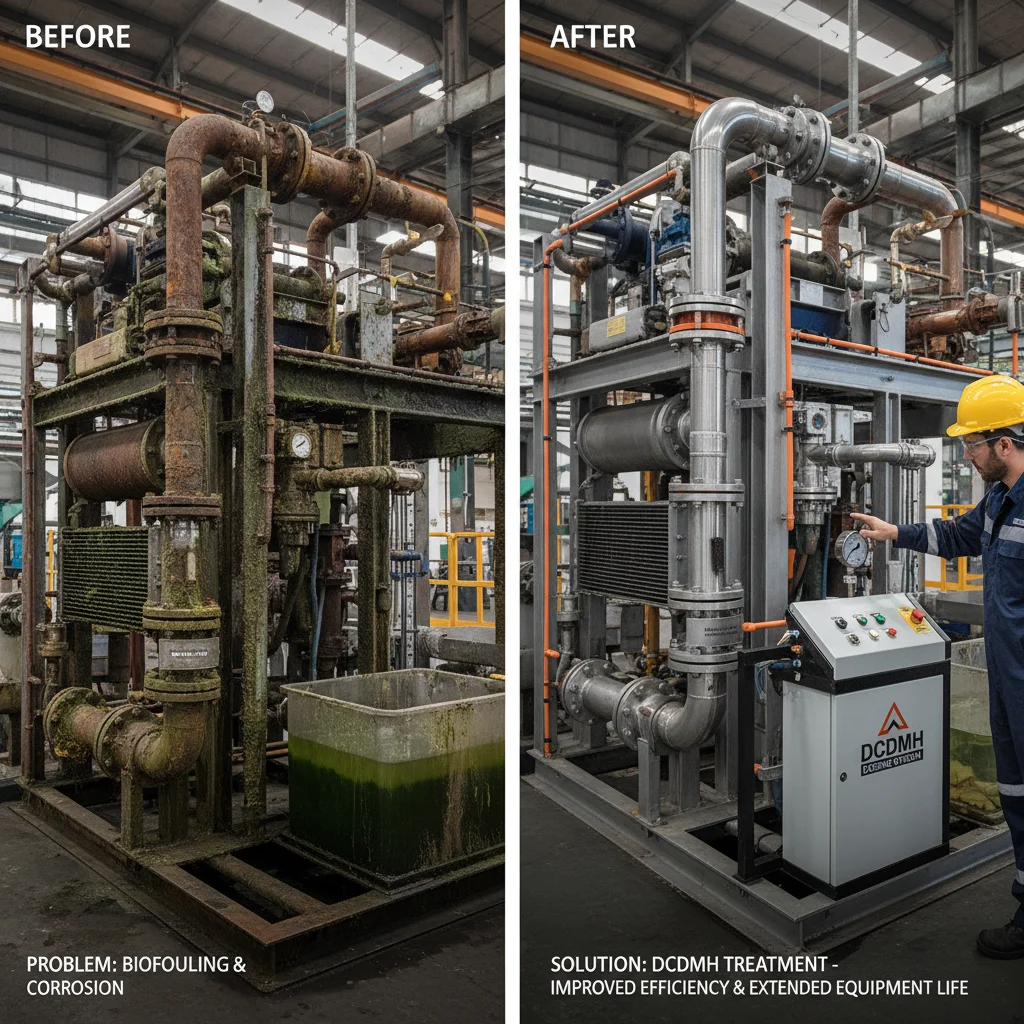
The output of a DMH factory extends far beyond the medical field, penetrating several high-growth industrial sectors. In the realm of water treatment, the compound is utilized as a potent biocide, helping to maintain hygiene standards in industrial cooling towers and pool and spa systems by inhibiting microbial growth.
Within the fine chemicals sector, the versatility provided by a professional DMH factory allows for the enhancement of coatings, adhesives, and agrochemicals. The molecular stability of the hydantoin ring ensures that the resulting products possess superior durability and performance characteristics.
Additionally, the compound's relevance has expanded into the electronics and personal care industries. Whether it is used as a stabilizing agent in specialized polymers or as a functional intermediate in cosmetic formulations, the consistent quality provided by a dedicated DMH factory is the foundation of product reliability.
Operational Efficiency and Scalability Factors
Scalability is a primary challenge in chemical manufacturing, and a sophisticated DMH factory addresses this by utilizing modular reactor systems. These systems allow for a seamless transition from laboratory-scale synthesis to full-scale industrial production without compromising the purity of the white crystalline powder.
Efficiency is further enhanced through automated dosing and temperature control systems, which minimize human error and ensure that every batch conforms to the established specification. This operational rigor is what separates a commercial-grade facility from a basic chemical plant.
Comparative Performance Ratings of DMH Factory Production Methods
Global Supply Chain and Packaging Logistics
The logistical capability of a DMH factory is just as important as its chemical expertise. To preserve the integrity of the white crystalline powder, particularly for sensitive pharmaceutical applications, moisture-resistant packaging is mandatory. Standard offerings include 25 kg fiber drums, which protect the product from atmospheric humidity and contamination during transit.
For large-scale industrial users, the facility provides 500 kg palletized containers and bespoke bulk formats. Every shipment is accompanied by rigorous quality check documentation, ensuring that the product adheres to international safety protocols from the moment it leaves the factory floor until it reaches the client's warehouse.
Future Trends in Hydantoin Derivative Production
The future of the DMH factory lies in the adoption of "Green Chemistry" principles. This involves the implementation of solvent-recovery systems and the reduction of hazardous by-products during the synthesis of 1,3-Dimethylol-5,5-Dimethyl Hydantoin, aligning the manufacturing process with global sustainability goals and ISO environmental standards.
Digital transformation is also reshaping the industry. The integration of AI-driven process control allows factories to predict potential deviations in purity in real-time, ensuring that the ≥99% purity threshold is never compromised, even during rapid production ramps.
Furthermore, there is a growing trend toward the synthesis of customized hydantoin derivatives. By leveraging the core technology of a DMH factory, manufacturers are exploring modified molecular structures to create even more specialized intermediates for the next generation of targeted oncology and neurology drugs.
Quality Control Frameworks in Chemical Manufacturing
A rigorous quality control (QC) framework is the heartbeat of any reputable DMH factory. Utilizing High-Performance Liquid Chromatography (HPLC) and Gas Chromatography (GC), the facility can verify the purity and moisture content of every batch. This analytical precision ensures that the product meets the high-value formulation requirements of pharmaceutical clients.
Beyond chemical analysis, the facility implements a comprehensive traceability system. Each drum of DMH is linked to a specific production batch, raw material source, and operator log, providing a transparent audit trail that is essential for FDA and EMA compliance in pharmaceutical manufacturing.
The final layer of quality assurance is the stability testing phase. By simulating various environmental conditions, the DMH factory ensures that the product maintains its crystalline structure and solubility over long-term storage, guaranteeing reliability for global distributors.
Core Quality Metrics for DMH Factory Production
| Analysis Dimension |
Testing Method |
Acceptance Standard |
Impact Level (1-10) |
| Chemical Purity |
HPLC Analysis |
≥ 99% |
10 |
| Moisture Level |
Karl Fischer Titration |
≤ 0.5% |
9 |
| Appearance |
Visual Inspection |
White Crystalline Powder |
7 |
| Solubility |
Solvent Compatibility Test |
Water/Organic Compatible |
8 |
| Contamination |
ICP-MS Trace Metals |
Below ppm limits |
9 |
| Packaging Seal |
Vacuum Leak Test |
Hermetically Sealed |
8 |
FAQS
A professional DMH factory prioritizes a purity level of ≥99% and a moisture content of ≤0.5%. These standards are critical for ensuring the stability of pharmaceutical intermediates used in API synthesis, preventing unwanted reactions and ensuring batch-to-batch consistency for pharmaceutical manufacturers.
To maintain stability, the factory utilizes moisture-resistant packaging such as fiber drums and palletized containers. Every shipment undergoes rigorous quality checks and is sealed according to international safety protocols to prevent hydration or contamination during global transit.
Yes, most advanced facilities provide tailored packaging options. While they handle bulk industrial orders in 500 kg containers, they also support R&D and pilot-scale production with smaller, bespoke formats to help laboratories accelerate their synthesis processes.
The compound is pivotal in pharmaceutical manufacturing (as an API intermediate), water treatment (as a biocide for pools and industrial systems), and fine chemicals (for adhesives and coatings). It is also increasingly relevant in the electronics and personal care sectors.
The compatibility with both water and organic solvents allows for immense flexibility in chemical synthesis. This means users can integrate the intermediate into various reaction environments without needing complex phase-transfer catalysts, simplifying the manufacturing workflow.
Purity is verified using advanced analytical instruments such as High-Performance Liquid Chromatography (HPLC) and Gas Chromatography (GC). These tests ensure the white crystalline powder meets the strict ≥99% purity requirement before it is cleared for dispatch.
Conclusion
The operational excellence of a DMH factory is fundamental to the success of modern pharmaceutical and industrial chemical synthesis. By maintaining a purity of ≥99% and adhering to strict moisture controls, these facilities provide the critical building blocks necessary for everything from life-saving medications to advanced water treatment biocides. The integration of rigorous quality control, scalable production methods, and specialized packaging ensures that 1,3-Dimethylol-5,5-Dimethyl Hydantoin remains a reliable and versatile compound for global industry.
Looking forward, the evolution of these factories toward green chemistry and digital automation will further enhance the sustainability and precision of hydantoin derivative production. For companies seeking a partner that combines technical expertise with a commitment to international quality standards, selecting a certified production facility is the most effective way to secure a stable and high-performing supply chain. Visit our website for more information: www.leache-chem.com